Food Grade Pet Bags: Safe for Food Contact Wholesale
A food-grade pet bag has one or more surfaces intended to contact food: a treat compartment, a removable bowl insert, a cooler lining, or a sealed snack pocket. The compliance requirement is that those surfaces are made from food-contact-approved materials and pass migration testing for the intended food type and contact time. Expect 9-22% above a standard build, at MOQ 500 pieces per colourway.
Food-contact claims convert a soft goods program into a regulated one, and the change is cheap to accommodate if it is planned and expensive if it is discovered late. Our production team builds food-grade pet bag programs at MOQ 500 pieces per colourway, with samples in 6-10 working days and bulk production in 35-50 days after approval, inspected to AQL 2.5 before release. The work has four parts. First, identify every surface that will contact food, including the ones designers do not think about, such as zipper tape next to a treat pocket or the inner face of a cooler lining. Second, specify food-contact-approved materials for those surfaces and only those surfaces, because blanket specification across the whole product costs money for no compliance benefit. Third, commission migration testing for the intended food type, contact temperature, and contact duration. Fourth, keep the supplier declarations and test reports in a file that a retail or marketplace reviewer can read in one pass. Buyers who follow that sequence move through review quickly; buyers who add a food pocket to an existing design after sampling usually restart the compliance clock and lose a season.
Wholesale heavy duty pet carrier builds start at the base panel, and Material & Technology documentation should state the board thickness before the fabric is chosen. Wholesale scratch resistant pet carrier and wholesale tear resistant pet carrier claims only hold when the test method is named, otherwise the coating alone is doing the work.
What Food Grade Means When a Pet Bag Has Food Contact
Food grade is not a property of the whole product. It is a property of specific surfaces that are intended to contact food, and everything else on the bag is judged as a general consumer article. That distinction is the single most useful thing a buyer can understand in this category, because it determines both the compliance scope and the cost. A pet bag with a sealed treat compartment has one food-contact surface; the shell, webbing, and hardware outside that compartment are not in scope.
The classification depends on intended use. A manufacturer and a buyer decide together which surfaces are intended for food contact, and that decision is recorded in the specification. A cooler lining intended to hold a sealed food pouch is a different case from a lining intended to hold loose food, and the second carries stricter requirements because contact is direct and prolonged.
Contact conditions define the testing. Regulators and testing houses work with three variables: the type of food, the temperature, and the duration. Fatty, acidic, and dry foods behave differently, and a material approved for dry contact may not be approved for fatty contact at temperature. Buyers should therefore write the intended use case into the specification before commissioning any test.
Buyers should also separate food contact from the adjacent claims that often arrive with it. A waterproof lining is not automatically food-safe, and a food-safe lining is not necessarily waterproof across a seam. Each property needs its own clause, and combining them in one requirement is how specifications become unquotable.
Food grade applies to the specific surfaces intended to contact food, for a stated food type, temperature, and duration, and the specification must state all three before any test is commissioned.
Which Components Actually Touch Food
Drawing the boundary correctly is the most common failure in these programs. The obvious surfaces are the interior of a treat compartment, the inner face of a removable bowl, and the lining of a cooler section. The missed surfaces are the ones adjacent to them: zipper tape and slider directly beside a food pocket, the binding tape that finishes the compartment edge, any printed label inside the compartment, and the seam sealant used on the compartment itself.
Hardware inside a food area also counts when contact is foreseeable. A snap or a rivet used to retain a bowl insert can contact food during use, and a buyer who specifies a food-safe lining with a standard plated fastener has created an uncontrolled surface. The rule is simple: anything inside the food zone that can be touched by food is in scope.
Adhesives and inks deserve their own line. An adhesive used to bond a lining, and any print applied inside a compartment, sit in the same regulatory category as the substrate. Specifying low-migration ink and a food-contact-appropriate adhesive is a small cost that closes a real gap.
Buyers should produce a short boundary list at design stage: a written inventory of every component inside the food zone with a material and a compliance status for each. That list becomes the basis for both the supplier declarations and the migration testing plan, and it is the document a reviewer asks for first.
A practical technique helps here: mark the food zone on the technical drawing with a closed boundary and require that every component crossing that boundary carries a compliance status in the bill of materials. Designers work visually, and a drawn boundary communicates the scope faster than a written clause. It also makes later design changes self-policing, because a new component added inside the boundary is obviously in scope, and the question gets asked during development rather than during a compliance review.
Finally, remember the accessories. A removable bowl, a scoop, or a liner bag shipped with the product is a separate article with its own status, and it should be specified and tested separately rather than assumed to be covered by the main product file.
Regulatory Frameworks a Buyer Has to Map
Food-contact rules are regional, and a buyer selling into several markets has to map them separately. In the United States, food-contact substances are regulated through a system of approvals and clearances administered at federal level, and a supplier declaration stating compliance for the intended use is the normal evidence. In the European Union, the framework regulation requires that materials do not transfer constituents to food in quantities that endanger health or change its composition, with specific measures for plastics and for other material groups.
Germany adds a national layer that is frequently requested by European buyers even outside Germany, because it is well known to retail compliance teams. China operates its own national standard series for food-contact materials, which matters both for domestic sale and for buyers whose supplier base operates there. Japan, South Korea, and other markets each add their own list.
The practical approach for a buyer is to name the destination markets in the specification and to ask the supplier for declarations matched to each. Asking for a generic food-safe statement is the mistake that costs time; asking for a declaration against the named framework for the named use produces a usable document on the first attempt.
Chemical compliance sits alongside food-contact rules rather than inside them. A lining can pass migration testing and still carry a substance restricted under REACH chemical requirements, so the buyer needs both files. Running the two screens together at sampling is cheaper than running them sequentially after a reviewer asks.
Where an article also carries a textile safety certificate, the evidence overlaps usefully. A OEKO-TEX textile safety certificate on the non-food surfaces supports the general product file while the migration reports cover the food zone, and together they answer most of the questions a retail reviewer will raise.
Migration Testing and What the Results Tell a Buyer
Migration testing measures how much of a material transfers into a food simulant under stated conditions. The report gives the buyer three things: whether the material passes for the intended food type, under what temperature and duration the pass holds, and which simulant was used. Reading those three lines carefully matters more than the pass itself, because a result obtained at room temperature for one hour does not support a claim about warm food held for a day.
Overall migration is the broad screen; it measures total transfer. Specific migration targets named substances and is required when a material contains a component with a known restriction. Buyers should ask which of the two was performed, because a report showing only overall migration may not satisfy a reviewer asking about a specific substance.
Testing should be commissioned per material and per colour where the colourant could migrate. A dark lining and a light lining of the same polymer can behave differently, and a buyer testing only the light version has an incomplete file. In practice most buyers test the darkest shade as the worst case plus the base material.
Buyers should also read the report for the contact story it tells rather than only for the pass line. A result covering dry food at ambient temperature for two hours does not support a product marketed for carrying warm food through a day of travel, even though both are food contact. Where the intended use is broader than the tested condition, the answer is to commission the broader test, not to interpret the narrower one generously. That distinction matters most in cooler linings, where chilled contact and ambient contact behave differently, and in compartments marketed for semi-moist treats, which sit between the dry and fatty categories.
Retesting cadence follows change control. Any change to lining material, coating, adhesive, or ink re-opens the question, and an annual refresh is a sensible default even without a change, because formulations drift and a reviewer will check the report date.
| Food-contact surface | Typical material | Cost index | Migration risk profile | Best use case |
|---|---|---|---|---|
| Treat compartment lining | TPU film | 130-165 | Low, tested for fatty and dry | Direct food contact, wipe clean |
| Removable bowl insert | Food-grade silicone | 180-260 | Very low, wide approvals | Direct contact, collapsible design |
| Cooler section lining | PEVA film | 110-140 | Low at chilled temperatures | Sealed pouches and chilled food |
| Compartment binding tape | Food-contact polyester | 105-125 | Low | Edge finish inside the food zone |
| Compartment zipper tape | Coated tape, declared | 115-145 | Medium, check coating | Closure adjacent to food |
| Interior print or label | Low-migration ink | +2-4% trim | Medium, screen per colour | Branding inside the compartment |
Read the cost index against the whole product rather than against the fabric. Food-contact materials usually represent a small share of the bill of materials, so a 150 index on a lining often moves FOB by only a few percent, which is why food-grade positioning is usually better value than buyers expect.
Material Choices for Food-Contact Surfaces
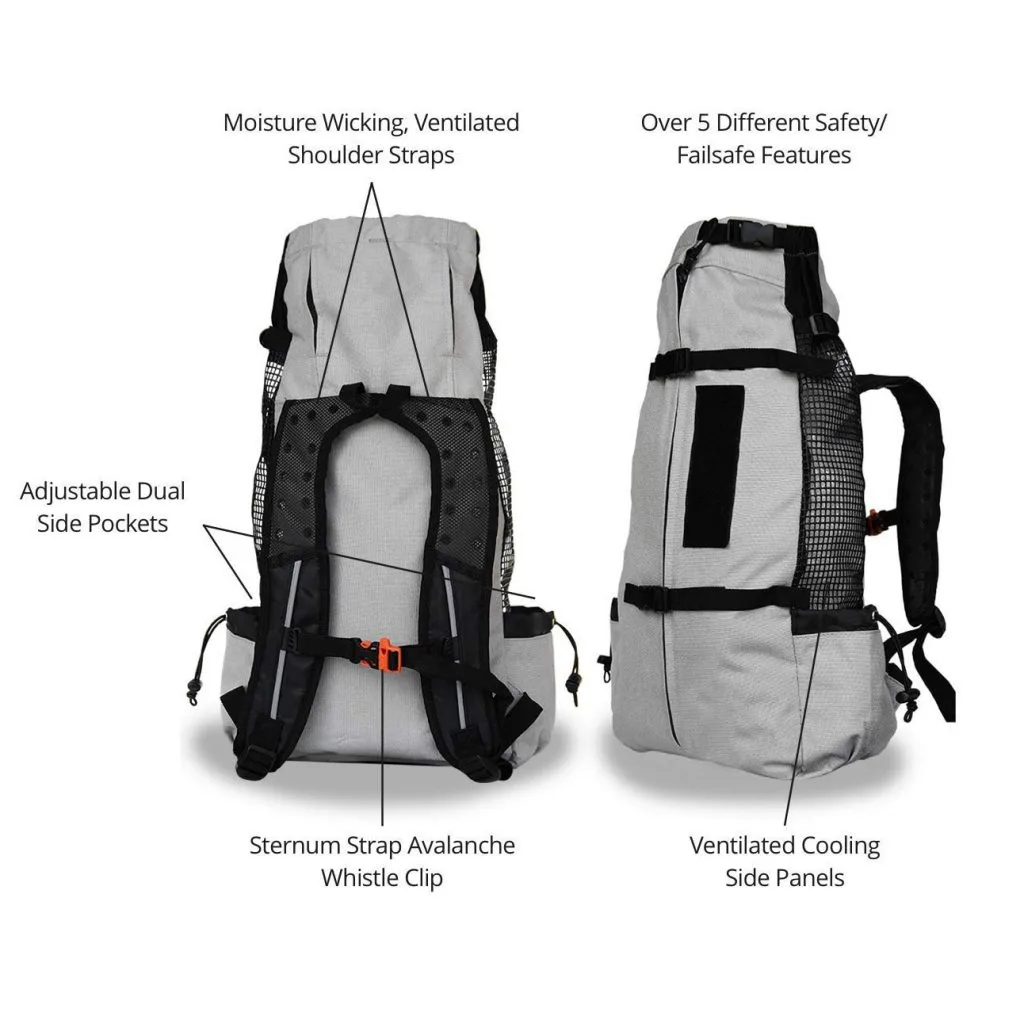
Three material families dominate food-contact surfaces in pet bags. Thermoplastic polyurethane films are the workhorse for compartments and linings: flexible, weldable, wipe-clean, and widely documented for food contact. Polyethylene vinyl acetate films are the chilled-food option, common in cooler sections and cheaper than TPU. Food-grade silicone is the premium choice for removable bowls and collapsible inserts, with the widest approval coverage and the highest cost.
Each has a processing implication a buyer should know. TPU welds well, which means a compartment can be made with sealed seams and no stitching, removing both a leak path and a compliance surface. PEVA welds but is less abrasion resistant, so it suits a cooler lining that is not rubbed daily. Silicone needs a different tooling approach entirely and is usually bought as a finished component rather than fabricated in the bag line.
Substrate choice for the surrounding product is unaffected. A pet bag can carry a standard polyester shell and a TPU-lined food compartment, and that is the cost-efficient configuration buyers should default to. Specifying food-contact materials across the entire product is a common and expensive misunderstanding.
Buyers should also verify the material's approval scope rather than its name. TPU as a family is not automatically approved for every food type, temperature, and duration; the specific grade and its declaration are what matter. Asking for the grade number and the declaration together is the fastest way to check.
Colour choice inside the food zone is worth a deliberate decision. Dark linings make stains less visible but typically carry more colourant, which is a migration consideration, while light linings show soiling and encourage cleaning. Most programs resolve this by using a mid tone with a tested worst-case shade, which balances the two pressures. Buyers should resist the temptation to match the compartment lining to the shell colour automatically, because doing so can force a retest of a shade that nobody evaluated.
Where a program also needs insulation, the insulated pet bag construction notes explain how the thermal layer and the food-contact layer are combined without putting the insulation inside the food zone.
Cost Structure of a Food-Grade Build
The direct material premium for a food-grade pet bag is modest, typically 9-22% at FOB when only the food-contact surfaces are upgraded. Silicone components sit at the top of that range and PEVA linings at the bottom. Because the upgraded area is usually a compartment or a lining rather than the whole product, the effect on total FOB is often in the low single digits to low double digits.
Testing is the larger and less predictable cost. Migration testing runs per material, per worst-case colour, and per intended food type, so a program with two food-contact surfaces, two simulants, and two colours can need a dozen reports. Modelled at 500 pieces that is significant; modelled across a multi-season program it is negligible. The planning implication is the same as in every compliance-heavy category: concentrate the first drop and plan the reorder.
Process cost appears in one place buyers overlook: welding equipment and sealing parameters. A welded compartment needs the right tooling and validated parameters, and a first run usually carries a setup cost. Suppliers running food-contact programs routinely amortise that across orders; suppliers encountering it for the first time quote it as a one-off charge, which is a useful signal when comparing quotations.
- Food-contact material premium: 9-22% on the affected surfaces
- Migration testing: per material, per worst-case colour, per simulant
- Welding tooling and parameter validation: one-off on first run
- Declaration collection: internal time, no fee
- Annual retest: recurring, modest
On the revenue side, food-grade positioning supports a price step and, more importantly, reduces a specific class of return. A compartment that stains, smells, or leaches generates the worst kind of review, and the testing spend is partly an insurance premium against that.
Documentation and Labelling for Food-Contact Claims
The documentation file has four elements: the boundary list of food-zone components, supplier declarations matched to the destination framework and intended use, migration test reports with conditions stated, and the internal change-control record. Presented together, they let a reviewer answer the question without correspondence. Presented separately, they generate a round of questions that usually costs two weeks.
Labelling should state the intended use plainly. Where a compartment is intended for dry treats, saying so is both a compliance statement and a usability improvement, and it prevents the misuse that leads to complaints. Symbols and statements recognised in the destination market are worth using, because a reviewer will recognise them without translation.
Care instructions belong in the same block. A food-contact surface needs cleaning guidance that does not degrade it, and a buyer should avoid recommending dishwasher or high-temperature cleaning unless the material and the construction have been validated for it. An unvalidated care instruction is a claim like any other.
Buyers should also decide how the claim reads on the listing. The defensible formulation names the material and its status, such as a food-grade TPU lining, rather than making a general safety promise. Marketplace reviewers respond better to a specific, traceable statement than to an adjective.
A food-contact claim survives review when the boundary list, the declarations, and the migration reports are presented as one file, because the reviewer then answers the question without asking the buyer anything.
Inspection and Production Controls for Food-Contact Programs
Production control for a food-contact program adds two requirements to a standard pet bag order. The first is material segregation: food-contact material must be identified and kept separate so that a substitution cannot happen silently. The second is seal validation: welded compartments need parameter control and a leak or seal check on the line, because a seal failure is invisible in a visual inspection and decisive in use.
Inspection at AQL 2.5 should name those checks. Seal integrity on food compartments, presence and legibility of the care and use labelling, and absence of odour in the compartment are all classifiable, and naming them in the worksheet is what turns them from observations into acceptance criteria. Our production team writes them in at order placement so the inspector and the buyer share a definition.
Independent verification is worth considering on a first program. A third-party inspection and testing provider can review declarations and reports alongside the physical inspection, which shortens the qualification cycle with a retail account and gives the buyer an unbiased record for the file.
Odour control deserves specific attention because it is the complaint most likely to reach a review page. A sealed-compartment odour check after ventilation, with a threshold agreed at sample approval, costs minutes per inspection and prevents the most damaging type of feedback in this category.
Finally, retain the production record. Lot identification for the food-contact material, mapped to cartons, allows a targeted response if a query arises, and it is the same control that makes every compliance program manageable rather than reactive.
Channel Fit and Order Planning
Food-grade positioning earns its cost in channels that sell on function and convenience: travel-oriented pet retail, outdoor and camping-adjacent pet ranges, and direct-to-consumer brands built around feeding routines. Those shoppers understand a treat compartment or a cooler section and will pay for a lining that is documented rather than merely claimed.
Discount channels rarely reward it, because the shopper compares capacity and price and reads food-grade as noise. The same compartment without the documentation is cheaper to build and easier to price, and buyers serving a price ladder should make that choice deliberately rather than paying for evidence that will not be read.
Order planning follows the standard wholesale model: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days after approval, AQL 2.5 inspection, T/T 30/70 terms, FOB Xiamen. The difference is the compliance clock, which runs in parallel with sampling and can be longer than the sampling window if testing is commissioned late. Starting declarations and test booking at quotation keeps the two clocks aligned.
Buyers should also plan the accessory decision early. A removable bowl or liner included with the product is a separate article with its own status, and deciding to include it after sampling restarts both the compliance and the tooling clock.
Where a program combines food contact with other compliance requirements, our guides to pet bag materials and REACH chemical compliance cover the overlapping parts of the file, and reading them together avoids duplicating tests.
Start the compliance clock at quotation rather than at sample approval, because migration testing and declaration collection routinely take longer than the sampling window itself.
Production capability
- SGS-verified production space of 4,950 m², 149 machines, 7 assembly lines
- Pet bag output since 2014 from a 137-person team
- 200,000 units shipped monthly under BSCI and ISO 9001 systems
People Also Ask
What makes a pet bag food grade?
Having surfaces intended to contact food made from food-contact-approved materials that pass migration testing for the stated food type, temperature, and duration. The rest of the product is judged as a general consumer article, so the requirement applies only to the designated food zone.
Which parts of a pet bag count as food contact?
The treat compartment lining, removable bowl insert, cooler lining, and also the adjacent components designers miss: zipper tape, binding tape, interior print, seam sealant, and any fastener inside the compartment that food can touch.
Does a food-grade pet bag need FDA approval?
In the United States the requirement is that food-contact substances are cleared or otherwise compliant for the intended use, evidenced by supplier declarations. It is not a product approval process, so the buyer collects declarations and migration reports rather than a certificate issued to the finished bag.
What is migration testing?
A laboratory measurement of how much of a material transfers into a food simulant under stated conditions. The report states the food type, temperature, and duration covered, and the buyer should check all three match the intended use before relying on the pass.
Is silicone better than TPU for food contact?
Silicone has wider approval coverage and suits removable bowls, but costs more and is usually bought as a finished component. TPU is the volume choice for linings and compartments because it welds well and is cheaper. The right answer follows the component, not the material reputation.
How much does food-grade construction add to cost?
Typically 9-22% on the affected surfaces, which usually translates to a much smaller move in total FOB because the food zone is a small part of the product. Testing is the larger cost and is fixed per program.
Can food-contact surfaces be stitched?
They can, but welding is preferable. Stitch holes create a leak path and add a compliance surface at the seam, while a welded compartment seals cleanly and removes both problems.
Frequently Asked Questions
Should the whole bag use food-contact material?
No. Specifying it across the entire product adds cost with no compliance benefit. The efficient configuration is a standard shell with food-contact materials only inside the designated food zone.
How many migration tests does a typical program need?
Per food-contact material, per worst-case colour, and per intended food simulant. Two surfaces, two simulants, and two colours can mean a dozen reports, which is why concentrating the assortment improves the economics.
Can a cooler lining hold loose food?
Direct contact with loose food carries stricter requirements than holding a sealed pouch. The specification should state which is intended, because the testing differs and a lining approved for one does not automatically cover the other.
Do care instructions need validation?
Yes. Recommending dishwasher or high-temperature cleaning is a claim about the product's tolerance, and it should only be stated after the material and construction have been validated for that condition.
What is the safest claim wording for a listing?
Name the material and its status, such as a food-grade TPU lining, rather than making a general safety promise. Specific and traceable statements survive marketplace review better than adjectives.
How often should migration testing be repeated?
Annually as a default, and immediately after any change to lining material, coating, adhesive, or ink. Reviewers check report dates, so a stale report is a weak answer even when nothing has changed.
What are the standard commercial terms?
MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days after approval, AQL 2.5 inspection, T/T 30/70, FOB Xiamen, with testing fees billed as program costs.
Is third-party inspection worth it here?
Yes on a first food-contact program. A provider can review declarations and reports alongside the physical inspection, which shortens qualification with a retail account and gives the buyer an unbiased record.
How should odour be controlled in a food compartment?
A sealed-compartment odour check after ventilation, with a threshold agreed when the approval sample is signed. That gives the inspector a reference for bulk rather than a subjective judgement later.
Does food contact change customs classification?
No. Classification follows the article and its material. The food-contact status affects compliance documentation, labelling, and listing content rather than duty treatment.
Should accessories be tested separately?
Yes. A removable bowl, scoop, or liner shipped with the bag is a separate article with its own status and should be specified and tested on its own rather than assumed covered by the main file.
What happens if a lining is substituted mid-program?
The migration reports no longer describe the product. A change-control clause requiring written buyer approval before any input change, plus lot identification, prevents this and keeps the file accurate.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample