Recycle-Ready Pet Bags: Material and Packaging Decisions
Recycle-ready describes a product that an existing sorting line can identify and that a recycler will actually buy, not a product made from a technically recyclable polymer. For wholesale pet bags the test is practical: one dominant polymer above roughly 90% of mass, separable or compatible trims, and a resin code that matches what the destination market collects.
Mono-material conversion is a design and trim exercise, and the buyer should cost it as one. Shell, lining, webbing, thread, and zipper tape moved into a single polymer family will change hand feel, abrasion behaviour, and price, so the comparison must be run on samples rather than on a specification sheet.
Commercial terms are MOQ 500 pieces per color, samples in 6-10 working days, bulk 35-50 days after sample approval, T/T 30/70, FOB Xiamen, and pre-shipment inspection at AQL 2.5. Add a sortability check - near-infrared identification, density separation, and trim removal - to the approval gate, and keep one conventional control sample so the performance trade-off is measurable rather than assumed.
Pet bag moq is quoted per colourway, not per order, so Material & Technology planning decides how many shades a launch can carry. A pet bag wholesale price that looks attractive at 500 units often shifts once the dye-lot minimum is added, and pet bag sample cost is normally credited back against the first production run.
Recycle-Ready Means a Sorter Can Identify It
Recyclability is not a property of a molecule; it is a property of a product inside a specific waste system. A polypropylene shell is recyclable where polypropylene is collected, sorted, and sold, and it is refuse where it is not. The buyer's first job is therefore to establish which stream the product will enter and whether that stream has a market for the output.
Three gates decide the answer. Collection: is the polymer accepted in kerbside or store drop-off in the destination market? Sorting: can the identification equipment on the line recognise the item and eject it into the correct bin? End market: does a reprocessor buy that material at a price that sustains the flow? Failing any one of the three makes the claim unsound, and the third is the one buyers most often omit.
Sorting is the most technical gate and the most commonly misunderstood. Modern material recovery facilities rely heavily on near-infrared spectroscopy, which reads the reflectance signature of a surface. A dark or carbon-black shell can be invisible to that equipment, and a multi-layer laminate returns a confused signal. Both outcomes send the item to residue regardless of what the polymer technically is.
Size and form matter as well. Small flexible items fall through screens and are lost to the residue stream in many facilities, and flat film behaves differently from rigid objects on a line. A pet bag is neither rigid nor large, which is a genuine constraint: it will often be better handled through a textile take-back or a store drop-off route than through kerbside mixed recycling.
Write the destination stream into the product brief. "Recycle-ready for store drop-off polyethylene film" is a different specification from "recyclable kerbside", and the first is frequently the honest one for soft goods.
Confirm the answer per market rather than per brand. A specification approved for one country cannot be assumed to work in the next, because collection lists, screening equipment, and end markets all differ, and the differences are not visible from a supplier quotation.
Mono-Material Design: Where It Works and Where It Breaks
Mono-material construction means the dominant polymer family accounts for nearly all of the mass, and the remaining parts are either the same polymer or easily separated. It improves sortability, it improves the value of the output, and it is the single most effective change a buyer can make. It also creates engineering problems that show up in sampling, so the decision should be made with a prototype in hand.
The usual approach is to move shell, lining, webbing, and thread into one family - polyester or polypropylene or polyethylene - and then work through the exceptions. Zipper tape is often nylon or polyester; sliders are metal or acetal; foam is polyurethane; base board is polyethylene, polypropylene, or paperboard; coatings and finishes add another chemistry. Each exception either converts, becomes separable, or stays and reduces the claim.
| Structure option | Polymer mix | Resin code | Identification on sorting line | Recycler acceptance | Cost delta per unit |
|---|---|---|---|---|---|
| Full polyester shell, lining, webbing, thread | Single family | 1 | Reads clearly | Good where PET stream exists | Baseline |
| Polyester shell with nylon zipper tape | Two families | 1 and 7 | Mixed signal | Downgraded or rejected | Zero |
| Polypropylene shell and board, PP webbing | Single family | 5 | Reads clearly | Variable by region | +2% to +5% |
| Polyethylene shell, PE foam, no metal | Single family | 4 | Reads clearly | Good where film collected | +3% to +7% |
| Laminated shell with PU coating | Multi-layer | 7 | Confused signal | Usually refused | Baseline |
| Conventional mix with riveted hardware | Three or more | 7 | Not viable | Residue | Baseline |
The cost column deserves a comment: mono-material is usually more expensive, not less, because it restricts the supplier to a narrower input set and sometimes requires a hardware redesign. The saving, if there is one, comes from simplification - fewer trim codes, fewer material lines to purchase and hold, and fewer substitution risks during bulk.
Where a full conversion is not viable, partial conversion still has value. Moving lining and thread into the shell polymer while leaving a metal slider is a meaningful improvement in sortability, and it can be described accurately as a step rather than as full recyclability. Buyers should resist the temptation to describe a partial conversion using whole-product language.
Resin Codes and What They Do Not Promise
The resin identification code is a numbering system for polymer identification, not a statement that an item is collected or recycled anywhere. A code of 1 on a component tells a sorter what the polymer is; it says nothing about whether the local authority accepts that item, whether the item is large enough to be captured, or whether there is a buyer for the output.
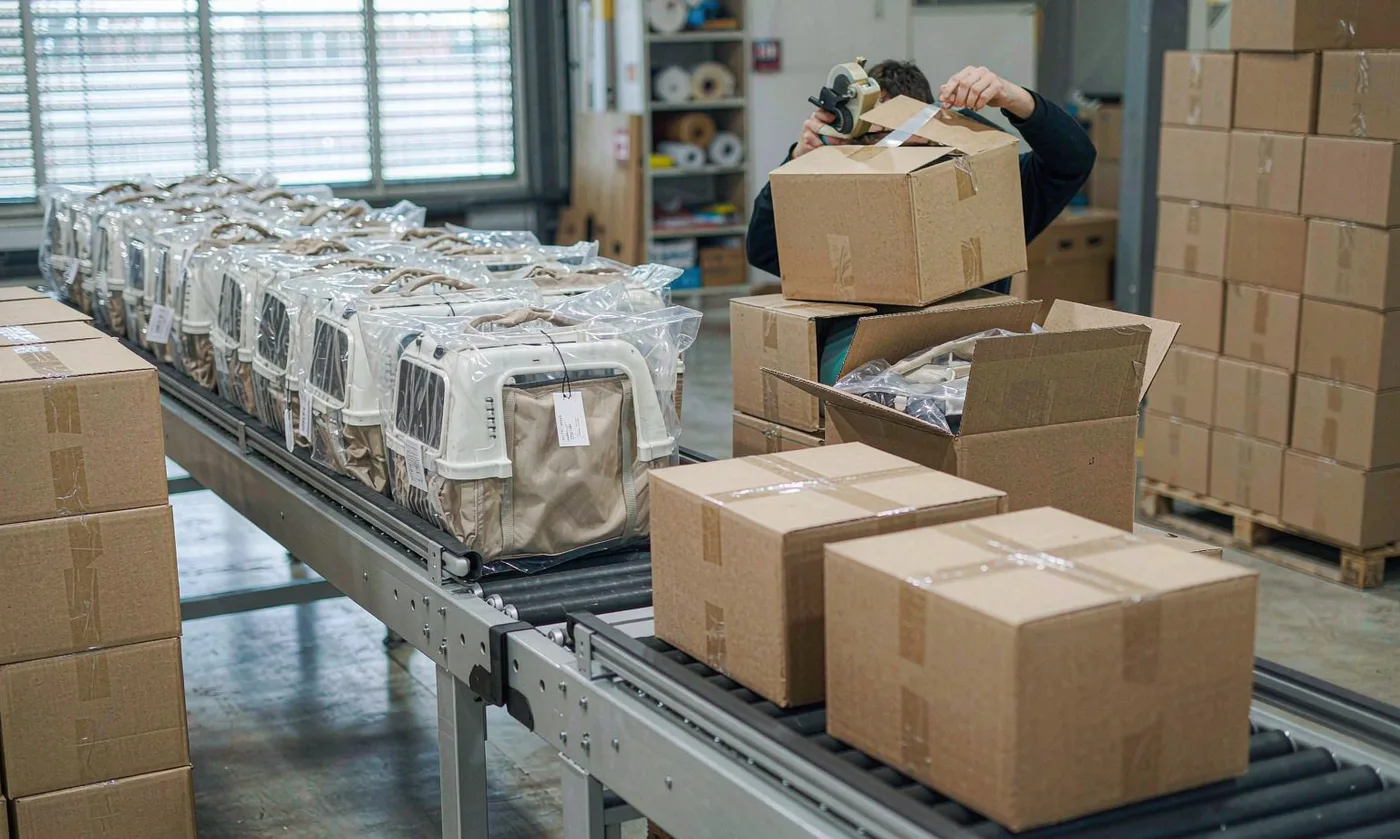
The system is maintained as a standard practice for coding manufactured articles, and the current version of that practice is published through ASTM International. Buyers should specify the code mark, its placement, and its size in the artwork file, because a code that is moulded in the wrong place or too small to read is functionally absent.
Placement rules are practical rather than aesthetic. Put the code on a flat, accessible face that will not be covered by a label or a hangtag. Avoid placing it inside a pocket or under a lining. Avoid colours that reduce contrast against the moulded surface. Then test it: photograph the part under warehouse lighting and confirm the number is legible at arm's length.
Use the code that matches the actual polymer, verified by the supplier's material declaration, not the code that matches the most collectable stream. Marking a polypropylene part as 1 because polyethylene terephthalate is more widely collected is mislabelling, and it contaminates the stream it was trying to join.
Where an item is genuinely multi-material, the honest marking is the other category rather than the code of the largest single polymer. That looks worse on a shelf and is better in a compliance file, and it also prevents the sorting line from being fed an item it will misidentify. Some buyers resist this because the number seven reads as failure; in practice, accuracy protects the claim.
Labels, Inks, Adhesives, and Small Parts
Recycling outcomes are frequently decided by the few percent of mass that is not the main polymer. Labels, inks, adhesives, coatings, and small hardware can each downgrade an otherwise clean stream, and each is specified by the buyer rather than determined by physics, which makes them the most controllable part of the problem.
Labels are the classic case. A paper label with a persistent adhesive on a polymer item can survive the wash process, discolour the output, and clog filters. Where a label is required, use the same polymer family as the substrate with a wash-off adhesive, keep coverage low, and confirm with the reprocessor or a recognised design guide what the threshold is.
Inks and coatings matter for the same reason. Heavy coverage, metallic pigments, and some durable water repellent treatments interfere with identification and with melt quality. Specify ink coverage as a percentage, name the pigment family, and require the supplier to declare whether the finish is applied to the whole surface or selected areas only. Keep that declaration in the compliance file.
Small parts are a sorting problem rather than a chemistry problem. Buckles, feet, and sliders below a few centimetres are lost during size screening and never reach the correct stream. Where a part is functional, accept the loss and record it; where it is decorative, delete it.
Substance compliance sits alongside all of this and is independent of recyclability. Materials entering the European market must satisfy restricted substance rules administered by the European Chemicals Agency, and recycled or recyclable inputs are not exempt. Keep the material declaration and the declaration of conformity together with the recycling file.
A practical way to keep this manageable is to set a small-part rule at the design stage: no component below a stated mass unless it performs a function, no adhesive where a stitch will do, and no coating where a tighter weave will do. Three rules, applied early, remove most of the contamination exceptions before they reach the component map.
Retailer and Marketplace Rules for Recycling Language
Channel requirements are where a technically sound specification meets a checklist, and the checklist is stricter than most buyers expect. Large retailers and marketplaces increasingly require a specific claim structure: what is recyclable, in which stream, in which geography, and with what evidence. Unqualified recyclable badges are being removed from listings across several platforms.
Prepare a standard response pack so every submission is identical. It should contain the polymer declaration by component with percentages by mass, the resin code and its placement, the identified destination stream, the collection coverage statement for the market, and any third-party assessment. Five documents, one folder per SKU.
Be careful with the phrase widely recycled. It is only defensible where collection coverage is genuinely high, and coverage numbers should come from a current published source rather than an assumption. Where coverage is partial, say kerbside in most areas or store drop-off, which is both accurate and, in practice, more useful to the shopper.
On-pack labelling schemes add another layer. Several markets operate standardised recycling label systems with their own artwork rules and eligibility criteria, and using a scheme label without meeting its criteria creates the same problem as using a certification mark without a licence. Confirm eligibility before the artwork is finalised, because a carton reprint is an expensive correction.
Expect the reviewer to ask about the component with the worst outcome, not the best. A submission that leads with the shell polymer and stays quiet about the foam base board will be picked apart, because compliance teams read the bill of materials before the marketing copy. State the exceptions up front and explain how each is handled; submissions that volunteer their weak points are approved faster than submissions that hide them.
Keep a version history for every claim submission. When a reviewer asks why a percentage changed between seasons, a dated record showing the material substitution behind it turns a suspicious discrepancy into a documented improvement.
Prove Sortability Before You Commit to Tooling
Sortability can be assessed before you invest in tooling, and it should be. Three checks are enough to separate a credible programme from a hopeful one: near-infrared identification on the finished surface, density behaviour in a float-sink test, and a manual separation trial timed with a stopwatch.
The near-infrared check is the important one, because it mirrors what the sorting line does. Submit finished samples - printed, coated, assembled - not raw fabric swatches, since print and finish change the reading. Where the equipment returns an unclear or wrong identification, the usual fixes are lighter colour, reduced coating, or a different surface texture.
The float-sink test confirms density separation, where the stream is separated by buoyancy. If the shell floats and the hardware sinks, the two can be split mechanically; if a laminate sits at an intermediate density, it will confuse the process. Record the result per component rather than per product.
The timed separation trial answers the economic question. If a person can strip the item into its streams in under two minutes, manual pre-processing is viable at some scale. If it takes ten minutes, it is not, and the claim should be reduced to whatever is genuinely separable.
Run all three on the approval sample and repeat them once on a bulk production unit. Agreement between the two is the evidence that the specification was actually followed, and a divergence is an early signal that an input was substituted during bulk.
Record the results as pass, marginal, or fail rather than as a narrative. Marginal readings matter most: an item that barely identifies on the line will be mis-sorted in a real facility, where items arrive dirty, crumpled, and moving fast. Treat a marginal result as a design instruction to lighten the colour or reduce the coating, and re-test before releasing the specification.
Costing the Conversion Against the Claim Value
Mono-material and recycle-ready specifications carry four cost elements: input premium, hardware redesign, testing, and inventory simplification. The first three push price up; the fourth can pull it down, and the net result is usually a modest increase that has to be justified by channel access rather than by margin.
Input premium comes from buying a narrower specification in smaller volume. Expect a few percent on fabric and more on specialised thread or tape. Hardware redesign is a one-off engineering cost that can often be amortised across a platform if several SKUs share the construction, which is the strongest argument for converting a family rather than a single style.
Testing is small in absolute terms but should be budgeted: identification testing, density checks, and any third-party assessment of the claim. Where several SKUs share a construction, one test programme can cover the platform, provided the component map is identical.
Inventory simplification is the offset. Fewer polymer families mean fewer trim codes, fewer material minimums to meet, and less dead stock at season end. Buyers who track working capital often find this is worth more than the input premium costs, particularly on a range with many colourways.
Commercial mechanics stay unchanged: MOQ 500 pieces per color, samples 6-10 working days, bulk 35-50 days after approval, T/T 30/70, FOB Xiamen, AQL 2.5 pre-shipment inspection. Add the sortability checks to the sample approval gate, and keep a conventional control so the merchandising team can see the hand-feel and abrasion trade-off rather than reading about it.
The final element is the price-position question: does the claim support a higher retail price, or does it merely preserve shelf access? In most pet categories the honest answer is shelf access, because retailer scorecards increasingly treat packaging and product claims as listing conditions. Budget the conversion as a cost of staying listed rather than as a margin opportunity, and the internal approval conversation becomes much shorter.
Write a Polymer Declaration Buyers Can Audit
The polymer declaration is the document that makes every other claim checkable. It lists each component, the polymer or material family, the mass in grams, the percentage of total mass, and whether the part is separable by hand. One page per SKU, versioned, dated, and signed off by the supplier's material manager.
Build it during sampling rather than afterwards, because the numbers change as the construction is refined and a declaration written at the end is usually an approximation. Weigh the parts from an approved sample rather than estimating from the pattern, and photograph the sample next to the list so the two can be matched later.
The declaration answers the questions that otherwise stall a retailer submission: what is the dominant polymer, what percentage does it represent, which parts sit outside the family, and how does a customer remove them. Four answers, one table, no prose required.
Tie the declaration to a change-control rule. Any substitution of fabric, thread, tape, foam, or hardware requires a new version and a re-check of the percentages, and the version number should appear on the inspection brief so the checker knows which document the goods are being measured against.
Where a buyer runs a platform of similar styles, one declaration can cover several SKUs provided the component map is identical and only colour differs. That shared document then supports one claim submission for the whole platform, which is the single largest saving available in this kind of programme.
Keep the declaration with the inspection file rather than in a marketing folder, because the two are read together: the checker verifies that the shipped construction matches the declared one, and the claim reviewer verifies that the claim matches the declaration. One document serving both purposes removes an entire category of internal contradiction.
Rolling the Specification Out Across a Wholesale Range
Convert one platform at a time, and start with the highest-volume style that already has stable tooling. That gives the largest absolute claim benefit for the smallest engineering risk, and it produces the sample evidence that makes the second and third conversion easier to approve internally.
Sequence the work. First the component map, so the exceptions are visible. Second the material substitutions, sampled and tested. Third the artwork and labelling changes, which depend on the final polymer declaration. Fourth the claim wording register, which cannot be written until the collection coverage for each destination market is confirmed.
Keep the conventional version in the range during the first season. It gives the sales team a fallback if the new construction is rejected on hand feel, it provides a price comparison that merchandising will ask for, and it de-risks the transition if a certified input becomes unavailable.
Quality management holds it together. A documented material change process under ISO 9001 quality management principles is what prevents a bulk substitution from quietly undoing the specification, and inspection at AQL 2.5 should include a check that polymer identity, resin code placement, and label construction match the approved file.
Our production team builds through partner facilities within an SGS-verified production base of 4,950 square meters with 137 people, 7 lines, 149 pieces of equipment, and about 200,000 pieces monthly capacity, and can hold lot-level material records for each conversion. The claim, the collection evidence, and the artwork approval remain the buyer's decisions to make and document.
Order and quality terms
- MOQ 500 pieces per colourway; samples in 6-10 working days
- Bulk production 35-50 days after approval; AQL 2.5 inspection standard
- T/T 30/70 terms, FOB Xiamen, full document set per shipment
People Also Ask
What does recycle-ready mean for a wholesale pet bag?
That an existing sorting line can identify the polymer, that the item survives size screening, and that a reprocessor will buy the output. All three must hold in the destination market.
Why are soft bags hard to recycle kerbside?
Flexible items are often lost in size screening and behave differently from rigid objects on a line, so store drop-off or take-back routes usually perform better than kerbside mixed recycling.
Which polymer family suits a mono-material pet bag?
Polyester suits shell, lining, webbing, and thread with good identification. Polypropylene and polyethylene are alternatives where the destination market collects those streams consistently.
What is the resin identification code standard?
A numbering practice for identifying polymer type in manufactured articles, maintained by ASTM International. It identifies material; it does not promise collection or recycling.
How much does mono-material conversion cost?
Expect a few percent more on fabric and more again on specialised tape or thread, offset partly by fewer trim codes and lower dead stock. Test the trade-off on samples before committing.
What documents do retailers ask for with a recycling claim?
Polymer declaration by component with mass percentages, resin code and placement, identified destination stream, collection coverage for the market, and any third-party assessment.
Should the first conversion cover one style or the whole range?
Start with the highest-volume style on stable tooling. Shared construction lets one test programme and one hardware redesign cover the rest of the platform later.
Frequently Asked Questions
What percentage of one polymer makes a pet bag recycle-ready?
A dominant polymer above roughly 90% of mass, with the remainder either the same family or hand-separable. Below that, sorting equipment returns a mixed signal and reprocessors downgrade or refuse the material.
Does a resin code mean the item is recycled locally?
No. The code identifies the polymer only. Local acceptance depends on collection coverage, item size on the sorting line, and whether a reprocessor buys that material.
Why does dark fabric cause sorting problems?
Near-infrared identification equipment reads surface reflectance, and carbon-black or very dark pigments can absorb the signal, sending the item to residue regardless of polymer.
Can a partial mono-material conversion be claimed?
Yes, but describe it accurately. Moving lining and thread into the shell polymer improves sortability; using whole-product recyclable language for a partial conversion does not.
How should resin codes be placed on a pet bag?
On a flat accessible face, not covered by a label or lining, with sufficient contrast and size to read at arm's length. Test legibility under warehouse lighting before artwork release.
Do labels and adhesives really affect recycling?
Yes. Persistent adhesives and paper labels can survive washing, discolour output, and clog filters. Prefer same-polymer labels with wash-off adhesive and keep coverage low.
What is the safest alternative to the phrase widely recycled?
Name the actual route, such as kerbside in most areas or store drop-off, and support it with a current published collection coverage figure for the destination market.
How is sortability tested before tooling?
Near-infrared identification on the finished printed surface, a float-sink density test per component, and a timed manual separation trial. Repeat on a bulk unit to confirm the specification held.
What sample and bulk timing applies to a conversion project?
Samples take 6-10 working days once materials are confirmed, and bulk runs 35-50 days after approval at MOQ 500 pieces per color. Hardware redesign may add one sample round.
Does recycled content help or hurt sortability?
Recycled content and sortability are separate attributes. A high-recycled-content item in a mixed-polymer laminate still fails identification, so evaluate each on its own evidence.
Should the conventional version stay in the range?
For the first season, yes. It provides a fallback if hand feel is rejected, a price comparison for merchandising, and protection if a specified input becomes unavailable.
What does AQL 2.5 inspection add for recycle-ready orders?
Verification that polymer identity, resin code placement, and label construction match the approved file. Define claim mismatches as defects before production rather than negotiating them at final inspection.
Is substance compliance separate from recyclability?
Entirely. Recyclable inputs must still satisfy restricted substance rules for the destination market, so keep the material declaration and conformity documentation with the recycling file.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample