Wholesale Cat Carriers: Shell Choices for Bulk Buyers
Short answer: wholesale cat carriers come in three shell classes: soft shell with 8-10 mm foam, semi-rigid EVA at 3-5 mm wall, and injection hard shell in PP or ABS at 2.5-3.5 mm. Soft shell gives the best carton cube and lowest tooling cost; hard shell gives the best stacking and impact resistance at four to six times the cube.
Shell choice is the decision that fixes everything downstream in a cat carrier programme: unit cost, tooling spend, carton cube, damage rate, shelf presentation and the compliance surface. It is also a decision most buyers make by looking at a photograph, which is the least reliable method available. This guide is written for importers, distributors and chain buyers specifying wholesale cat carriers at container volume, where a shell decision made casually costs more than any price negotiation recovers. QUANZHOU JUNYUAN BAGS has run pet bag programmes since 2014, with a founder in the trade since 2004, working to a fixed commercial frame: MOQ 500 per colourway, samples in 6-10 working days, bulk production 35-50 days after sample approval and deposit, AQL 2.5 final inspection, T/T 30/70 and FOB Xiamen. Our production team operates from an SGS-verified production base of 4,950 square metres with 7 lines, 149 machines and 137 staff at roughly 200,000 pieces monthly under BSCI and ISO 9001. The eight sections below compare shell classes on structure, tooling, ventilation, freight, failure modes and range strategy. Decide the shell before you decide the colourway.
Bulk pet bag orders consolidate best when carton dimensions are fixed early, and Pet Bag Types & Styles decisions are what fix them. Bulk pet carrier orders that mix sizes inside one carton save freight but complicate the packing line, so the trade-off should be priced rather than assumed.
What Shell Actually Means in a Cat Carrier Specification
In this category the word shell is used loosely to mean everything from a fabric bag with a foam insert to a rigid moulded box, and the looseness causes specification errors. A shell is the component that holds the carrier's shape under load and resists external force. It may be fabric plus foam, a moulded panel, or an injection-moulded structure, and each behaves differently in production, in transit and in use.
The three questions that define a shell are: what holds the shape, what resists compression, and what happens when the carrier is dropped or stacked. A soft shell answers all three with fabric tension and foam thickness. A semi-rigid shell answers with a moulded panel that flexes and recovers. A hard shell answers with a rigid structure that resists and may crack. All three are legitimate; they suit different channels and different price points.
Cats place a specific demand on the shell that dogs do not: they resist being loaded, and they apply force from inside with claws and with body weight against a confined surface. A shell that is adequate for a compliant dog can be inadequate for a resistant cat, not because the cat is heavier but because the load is applied differently and concentrated at panels and closures.
That distinction should be stated in the specification rather than assumed. Where a product is sold as a cat carrier, the closure, the panel attachment and the ventilation apertures should be tested for a resisting animal, and the test method should be written down. Generic soft-goods testing does not cover it.
The second specification point is that shell choice is not reversible within a season. Tooling, patterns, cutting dies and carton specifications are all built around it. A shell change mid-programme means a new development cycle of 6-10 working days per sample round and a new carton cube, which means a new container plan. Decide once, at the start.
Soft Shell: Fabric, Foam and the Semi-Structured Frame
Soft shell is the default for value and mid-tier cat carriers and it remains the highest-volume construction in most import markets. The structure is an outer fabric, a foam layer, an optional frame element at the base and sometimes at the opening, and a lining. Shape retention comes from the interaction of those layers rather than from any single rigid part.
| Shell class | Wall or foam thickness (mm) | Typical unit weight (g) | Pieces per carton | Carton cube (m3) | Tooling cost |
|---|---|---|---|---|---|
| Soft shell, flat-packed | 8-10 foam | 650-950 | 16-20 | 0.084-0.103 | None beyond dies |
| Soft shell, framed base | 10-12 foam | 900-1,250 | 12-16 | 0.103-0.131 | Dies only |
| Semi-rigid EVA | 3-5 wall | 1,200-1,800 | 6-8 | 0.140-0.170 | Low mould cost |
| Hard shell PP | 2.5-3.5 wall | 1,800-2,600 | 4-6 | 0.190-0.230 | High mould cost |
| Hard shell ABS | 2.5-3.0 wall | 2,000-2,900 | 4-6 | 0.190-0.230 | Highest mould cost |
Foam thickness is the variable that matters most in a soft shell and the one least often specified. At 8 mm the carrier holds a shape but feels soft; at 12 mm it feels substantial and costs more in both material and cube. Specify the thickness and the density together, because a thick low-density foam compresses permanently and a thin high-density foam feels hard but holds shape.
The frame element is the second decision. A removable base board is standard and expected; a frame at the opening, usually a wire or a moulded strip, is what stops the mouth of the carrier collapsing when the animal leans against it. Buyers omit it to save cost and then discover it in the return rate rather than in the unit price.
Fabric choice interacts with the shell. A heavier denier with a coating adds structure but reduces breathability and adds weight; a lighter fabric needs more foam to achieve the same feel. The balance should be struck against the price point rather than chosen independently, and the material basis should be written into the specification so it cannot drift.
Soft shell also offers the best nesting and flat-pack potential of the three classes, which is the reason it dominates in programmes where freight cost per unit is the binding constraint. Recovering a third of the cube through flat packing is achievable here and essentially impossible with a hard shell.
Semi-Rigid: EVA and Moulded Panel Constructions
Semi-rigid occupies the middle of the market and is the most technically interesting of the three classes. A moulded EVA panel or a set of moulded inserts gives a defined shape that recovers after compression, without the full rigidity and weight of an injection shell. The result presents well on shelf and protects better than fabric alone.
Wall thickness in the 3-5 mm range is the working band. Below 3 mm the panel is floppy and offers little advantage over foam; above 5 mm the weight and the material cost rise sharply without a matching increase in perceived quality. Ribs and geometry do more for rigidity than raw thickness, and a well-ribbed 3 mm panel outperforms a flat 5 mm one.
Mould cost for EVA is substantially lower than for injection moulding, because the tooling is simpler and the cycle is different. That makes semi-rigid viable at lower volumes than hard shell, and it makes it the natural choice for a buyer who wants a structured presentation but cannot amortise an injection tool across the forecast.
There are two production risks specific to this class. The first is panel-to-panel joins: a moulded panel attached to a fabric body creates a seam that has to carry load, and it is the most common failure point. Specify the attachment method, the stitch density and whether the join is reinforced, and check it on the golden sample under load rather than by looking at it.
The second is recovery. EVA panels that are compressed for a long transit, or stored stacked under weight, can take a set that does not fully recover. Ask what the recovery specification is and how long the panel can remain compressed, then set a warehouse stacking rule accordingly. This is a storage question as much as a product question.
Where a buyer is running both wholesale cat carriers and wholesale dog carriers in one programme, semi-rigid is often the shared platform: the panel geometry scales, the tooling is affordable, and the presentation looks consistent across the two species lines on shelf.
Hard Shell: PP, ABS and the Economics of Injection Tooling
Hard shell is the premium presentation and the most capital-intensive choice. An injection-moulded PP or ABS structure gives rigidity, cleanability, stacking strength and a distinctly higher perceived value. It also commits the buyer to a tooling investment and to a carton cube that is four to six times that of a flat-packed soft carrier.
PP is the workhorse material: lighter, cheaper, more flexible, and more forgiving in impact because it deforms rather than cracks. ABS is stiffer, takes a better surface finish and holds paint and print better, but it is heavier, more expensive, and more prone to visible cracking under sharp impact. For a carrier that will be dropped and stacked, PP is usually the better engineering choice despite the lower perceived finish.
Wall thickness in the 2.5-3.5 mm range is standard. Thinner walls save material and weight but introduce sink marks and reduce stacking strength; thicker walls add cost and cycle time without much benefit. Uniform wall thickness matters more than the absolute figure, because variable thickness is what causes warpage in a moulded part.
The tooling economics are the real decision. A set of moulds for a carrier shell is a five-figure investment in most cases, and it has to be amortised across the forecast. At a minimum of 500 pieces per colourway, a single colourway will not amortise a tool; the calculation has to run across the whole programme life, including reorders, before the decision is sound.
Tooling ownership should be settled at the point of payment, in writing, with the moulds identified and tagged. A buyer who has paid for tooling without documenting ownership will discover the problem when they want to move the programme, at which point the tooling is effectively a hostage.
Finally, ask about mould maintenance and cavity life. A tool has a finite number of cycles before refurbishment, and the cost of refurbishment should be allocated in the unit price rather than invoiced as a surprise in year three. Material and safety test methods referenced to ASTM standards give a common language for comparing impact and rigidity claims between two quotes.
Ventilation, Visibility and the Constraints Specific to Cats
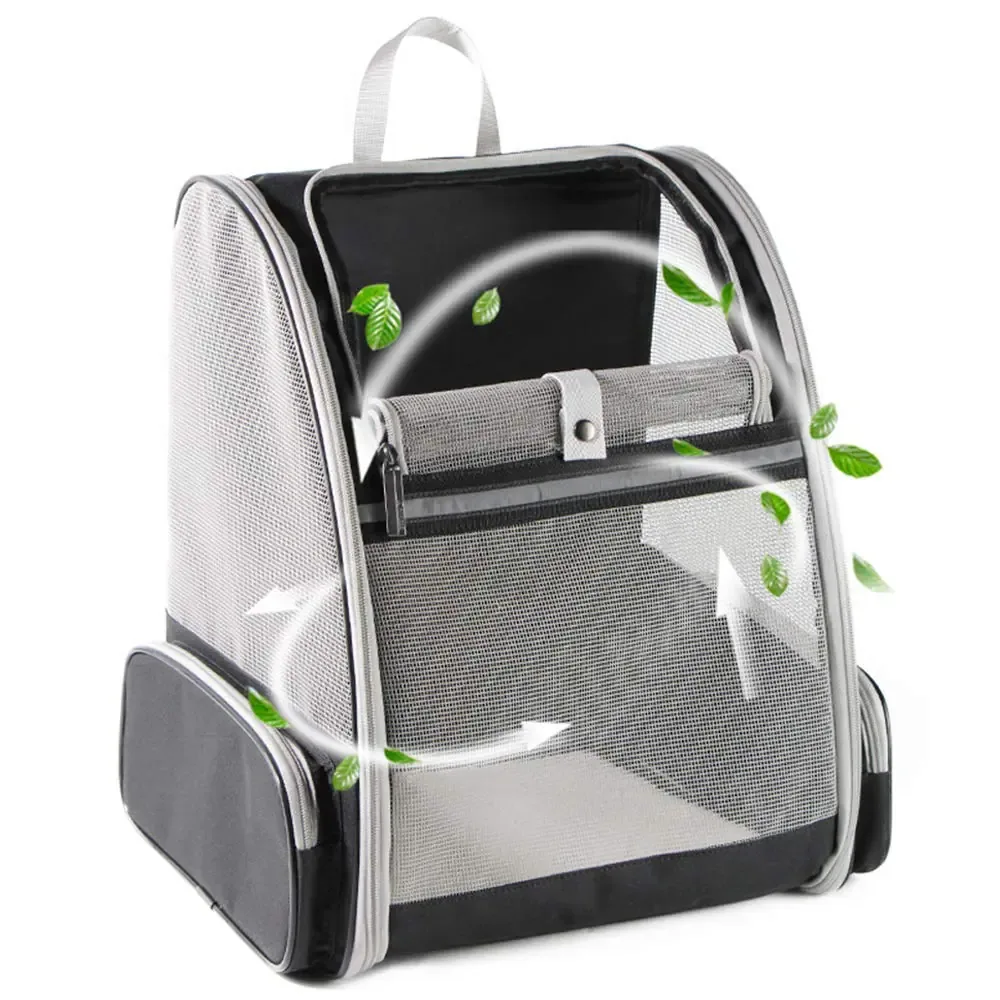
Ventilation is a shell decision because the apertures are cut through the shell, and every aperture removes structure. The engineering problem is to provide adequate airflow across the carrier's cross-section without creating a panel so perforated that it loses shape or a mesh so large that it becomes a claw-catch and an escape risk.
The practical target is ventilation on at least three faces, with the largest area on the faces least likely to be blocked in use. A carrier with generous top ventilation and nothing on the long sides performs badly when it is carried against the body or placed on a seat, because both block the top. Cross-flow matters more than total aperture area.
Mesh specification deserves its own line. A tight woven mesh resists claws better than a large-aperture net, and a bonded or welded mesh attachment holds better than a sewn one at the aperture edge. Specify mesh type, aperture size and attachment method, and check the attachment under a pulling load rather than visually.
Visibility is a commercial rather than a safety feature, but it drives conversion. Cats settle better when they can see out, and owners buy the carrier that lets them. A transparent panel in a hard shell or a large mesh window in a soft shell both sell better than an opaque box, provided the aperture does not compromise the structure.
Closure is the last cat-specific constraint and the one most often under-engineered. A cat that does not want to be loaded tests the zipper, the panel edge and any gap at the aperture. Specify zipper grade, whether there is a secondary closure, and whether the aperture can be opened from outside against resistance. General product safety obligations in the US market are summarised by the Consumer Product Safety Commission, and pet-specific containment guidance is published by the Center for Pet Safety.
How Shell Choice Propagates Into Freight and Warehouse Cost
The freight consequence of shell choice is large enough to change the ranking of two quotations. A flat-packed soft shell at 20 pieces per carton and a nested hard shell at 5 pieces per carton differ by a factor of four in units per cubic metre, and freight is frequently 10-25 percent of landed cost in this category. Comparing FOB prices without the cube adjustment produces the wrong answer.
The warehouse consequence is equally large and less often modelled. A hard shell carrier occupying four times the cube per unit occupies four times the shelf and four times the warehouse slot. For a distributor holding six months of cover, that difference is a real occupancy cost that belongs in the margin calculation rather than being absorbed silently.
Damage rate runs the other way. Hard shell protects better in transit and in a distribution centre, so the higher cube is partly offset by fewer damaged units and fewer claims. The offset is real but it is usually smaller than the cube penalty, which is why soft and semi-rigid dominate at value price points and hard shell concentrates at premium ones.
Pallet and stacking behaviour differ too. Hard shells stack cleanly and can be palletised to greater height without crushing, which recovers some warehouse cube. Soft shells cannot be stacked as high and need shelf or bin storage, which is cheaper per unit of product but more expensive per unit of space in a high-rent market.
The net calculation should be done once per programme: landed freight per unit plus warehouse occupancy per unit minus expected damage cost per unit. Buyers who run it usually conclude that a mixed shell strategy is right, with soft shell carrying volume and hard shell carrying margin, rather than committing the whole range to one class.
Failure Modes by Shell Type and How to Test for Them
Each shell class fails in a characteristic way, and each failure mode has a corresponding test that can be run on a golden sample rather than discovered in the market. Knowing the pattern turns quality from a hope into a specification.
Soft shells fail at the seams and at the base board. The characteristic failure is a strap root pulling away from the body under load, or a base board that folds rather than supporting, because the board pocket is too loose or the board density is too low. Test by loading the carrier to the top of its stated band and lifting by each carry point in turn, then check the board under a point load.
Semi-rigid shells fail at the panel-to-fabric join and through panel set. The join tears under load; the panel takes a permanent compression from stacking. Test the join with a pull test on a sample and test the panel by compressing it under a defined weight for a defined period and measuring recovery. Both are cheap and both are routinely skipped.
Hard shells fail by cracking and by closure failure. A drop onto a corner at low temperature is the classic test, and PP and ABS behave differently under it. Test the closure separately by applying an outward force from inside the aperture, which is a reasonable simulation of a resisting animal and is not covered by any standard soft-goods test.
Zippers fail across all three classes and are the most common single defect. Specify a cycle rating, require a pull test on the slider and tape, and check the zipper on the golden sample under the load case rather than unloaded. A zipper that runs smoothly empty can jam under tension.
Record the test method and the acceptance criterion in the specification, and require the results on the golden sample rather than on production. AQL 2.5 governs the production run; the sample tests govern whether the design is sound in the first place. Both are needed, and confusing them is how a design defect ships in a compliant run.
Choosing a Shell Strategy Across a Whole Cat Range
A range does not need one shell class, and the best-performing ranges usually do not have one. The decision should be made per band and per price point rather than globally, because the right shell for a value opening-price carrier is not the right shell for a premium travel product.
A common and effective structure is three tiers. Value tier uses soft shell with flat packing, maximising cube and hitting the opening price point. Mid tier uses semi-rigid EVA, giving structure and shelf presence at an affordable tooling cost. Premium tier uses hard shell in PP, carrying margin and justifying the tooling across a multi-season programme.
The middle tier is where most programmes under-invest. It is the tier with the best margin-to-risk ratio, because the tooling is modest, the presentation is strong and the cube penalty is half that of hard shell. Buyers who jump from soft straight to hard shell miss it, and they carry a cube penalty they did not need to accept.
Across tiers, standardise what can be standardised. Shared hardware, shared lining, shared webbing and shared colour references reduce the number of material lots, reduce the effective minimum per component and make the range look coherent on shelf even where the shells differ.
Then plan the shell decision into the calendar honestly. Hard shell adds tooling time before the sample cycle starts, and semi-rigid adds mould lead time. Both sit outside the 6-10 working day sample window and the 35-50 day bulk window, so they must be added to the timeline rather than assumed inside it. Programmes that plan for this land on time; programmes that discover it land into the season.
Specifying a Shell So It Survives the Third Reorder
A shell specification is written once and relied on for years, and the failure mode is drift rather than catastrophe. By the third reorder the foam density has quietly changed, the panel supplier is different, the wall thickness sits at the bottom of the tolerance and the carton cube has grown by five percent. None of those is a defect on its own, and all of them are recoverable if the specification was written tightly enough to detect them. Wholesale pet carrier programmes that skip this step usually discover the drift as a returns pattern rather than as a measurement.
The control is a shell specification sheet with measured values and tolerances rather than descriptions: foam thickness in millimetres with a tolerance, foam density as a number, panel wall thickness per zone, material grade and melt behaviour for moulded parts, mesh specification and attachment method, and a closure component rating. Each can be verified on one sample in an afternoon, and each is the kind of detail that drifts when nobody is measuring. Any buyer who will buy pet carriers at container volume should insist on the sheet before the first deposit.
Require a shell sample from production rather than from development on each reorder. A development sample is made slowly by the best operator; a production sample is made at rate. Comparing the two on the third order is the cheapest way to find out whether the specification has been followed, it costs one unit and one photograph, and it is also the only reliable check on a pet carrier wholesale platform shared across several markets.
Moulded parts have a specific maintenance dimension. Injection tools have a cavity life, EVA tools have a wear profile, and both produce parts that drift out of tolerance before they fail visibly. Ask for the cavity count at each shipment and agree who pays for refurbishment, because the answer belongs in the unit price rather than in an invoice three years in.
Buyers running cat and dog lines in parallel should hold both shell specifications in the same format, because the drift patterns are comparable and a single review catches both. A wholesale dog carriers programme sharing a platform with cat shells benefits most from a common foam and hardware specification, and a bulk dog carriers order quoted off that platform reduces the number of material lots. The same discipline applies to any bulk pet carriers programme spanning several markets, and it is why a written specification outperforms a good relationship: relationships forget, specifications do not. Material documentation follows the approach in quality assurance, and defect thresholds follow defect rate standards.
Why brands source here
- Pet bag programmes run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
What is the best shell material for a wholesale cat carrier?
There is no single best; the right choice depends on price point and channel. PP hard shell at 2.5-3.5 mm gives the best impact and stacking performance, semi-rigid EVA at 3-5 mm gives the best balance of presentation and cost, and soft shell with 8-10 mm foam gives the best freight cube.
How thick should carrier foam or shell wall be?
Soft shell foam works at 8-12 mm, semi-rigid EVA wall at 3-5 mm, and injection hard shell wall at 2.5-3.5 mm. Specify thickness with density or material grade, because thickness alone does not determine performance.
Is hard shell worth the tooling cost?
Only if the tooling amortises across the whole programme life including reorders. A single colourway at 500 pieces will not amortise a five-figure mould set, so the calculation must run across several seasons before hard shell is justified.
Why do cat carriers need different testing than dog carriers?
Cats resist loading and apply force from inside with claws and body weight against panels and closures. That load case is not covered by generic soft-goods testing, so closure strength, mesh attachment and aperture integrity need their own checks. Buyers who buy dog carriers in bulk should specify shell thickness separately per species, and the same applies to bulk pet carriers orders placed off the same platform.
How much does shell choice affect freight cost?
Substantially. A flat-packed soft shell can reach four times the units per cubic metre of a nested hard shell, and freight is often 10-25 percent of landed cost, so two quotations cannot be compared on FOB price alone.
Who owns the injection moulds?
Whoever paid, which should be documented at the point of payment with the moulds identified and tagged. Without that record, moving a programme in year three becomes a redevelopment rather than a transfer.
Frequently Asked Questions
What is the difference between PP and ABS shells?
PP is lighter, cheaper and deforms under impact rather than cracking, making it the better engineering choice for a carrier that will be dropped. ABS is stiffer, finishes better and holds print, but is heavier and more prone to visible cracking. Bulk dog carriers programmes using the same tooling family should specify the material per part rather than per programme.
Can a hard shell carrier be nested for shipping?
Partly. Nesting recovers roughly 30-45 percent of cube if the shell geometry has a draft angle designed for it, and it must be designed into the mould from the start rather than attempted afterwards.
How much ventilation does a cat carrier need?
Apertures on at least three faces with genuine cross-flow. Total aperture area matters less than placement, because a carrier carried against the body or placed on a seat has its top ventilation blocked.
What mesh specification resists cat claws?
A tight woven mesh with a bonded or welded attachment at the aperture edge. Large-aperture netting catches claws, and sewn mesh edges are the most common point of failure under a pulling load.
Do moulded EVA panels recover after compression?
Usually, within a defined limit. Ask for the recovery specification and the maximum recommended compression period, then set a warehouse stacking rule that respects it, because long compression under weight can produce a permanent set.
Should the base board be removable?
Yes, it is expected at most price points and it also helps flat packing. Specify the board density and the pocket tolerance, because a loose pocket lets the board fold under point load.
How do I test a carrier closure properly?
Apply outward force from inside the aperture rather than pulling the zipper empty. That simulates a resisting animal and is not covered by any standard soft-goods test, which is why closure failures reach the market.
What causes sink marks and warpage in moulded shells?
Non-uniform wall thickness. Variable sections cool at different rates and pull the part out of shape. Uniform wall within the 2.5-3.5 mm band matters more than the absolute figure chosen.
Is a mixed shell strategy better than one shell class?
Usually. Soft shell carries volume and hits the opening price point, semi-rigid carries margin with modest tooling, and hard shell anchors the premium tier. Committing a whole range to one class typically sacrifices either volume or margin. Buyers who buy pet carriers wholesale across two channels usually need two shell classes rather than one compromise.
How does shell choice affect warehouse cost?
Directly, through cube per unit. A hard shell occupying four times the cube of a flat-packed soft shell occupies four times the shelf and warehouse space, which is a real occupancy cost for a distributor holding months of cover. Wholesale pet carrier ranges built on three shell classes need three separate storage profiles.
Does tooling time fit inside the normal sample window?
No. Mould and tool lead time sits outside the 6-10 working day sample window and the 35-50 day bulk window, so it must be added to the programme timeline rather than assumed inside it. Anyone who will buy dog carriers in bulk on a fixed retail calendar must add tooling lead time before the sample window even opens.
What should be standardised across a multi-shell range?
Hardware, lining, webbing and colour references. Sharing these reduces material lots, lowers the effective component minimum and keeps the range visually coherent on shelf even where the shell classes differ. A pet carrier wholesale programme standardised on hardware can move shells without re-testing every component.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample