Pet Bag Manufacturer: Complete Sourcing Guide
Short answer: qualify a pet bag manufacturer on four numbers before you discuss price — MOQ 500 pieces per colour, 6-10 working days for a development sample, 35-50 days for bulk production, and AQL 2.5 as the final random inspection standard. A supplier that promises 100-piece runs, three-day samples and no inspection protocol is almost always reselling stock rather than running a managed program.
This guide is written for importers, distributors and retail buying teams that need repeatable wholesale pet bag programs instead of one-off spot purchases. Our production team plans capacity from an SGS-verified production base of 4,950 square metres running 7 lines with 149 machines and 137 staff, which supports roughly 200,000 pieces of monthly output across travel bags, totes, slings, backpacks and rolling duffels. Standard commercial terms are MOQ 500 pieces per colour, 6-10 working days for sampling, 35-50 days for bulk production after sample approval and deposit, AQL 2.5 final random inspection, T/T 30/70 payment, and FOB Xiamen as the default Incoterm. Certification coverage includes BSCI and ISO 9001, with third-party testing arranged through SGS for CPSIA, REACH, Prop 65 and OEKO-TEX where the destination market requires it. Work through the process in order: write the specification, understand the cost drivers, lock the sample, book capacity, then inspect before releasing the balance payment.
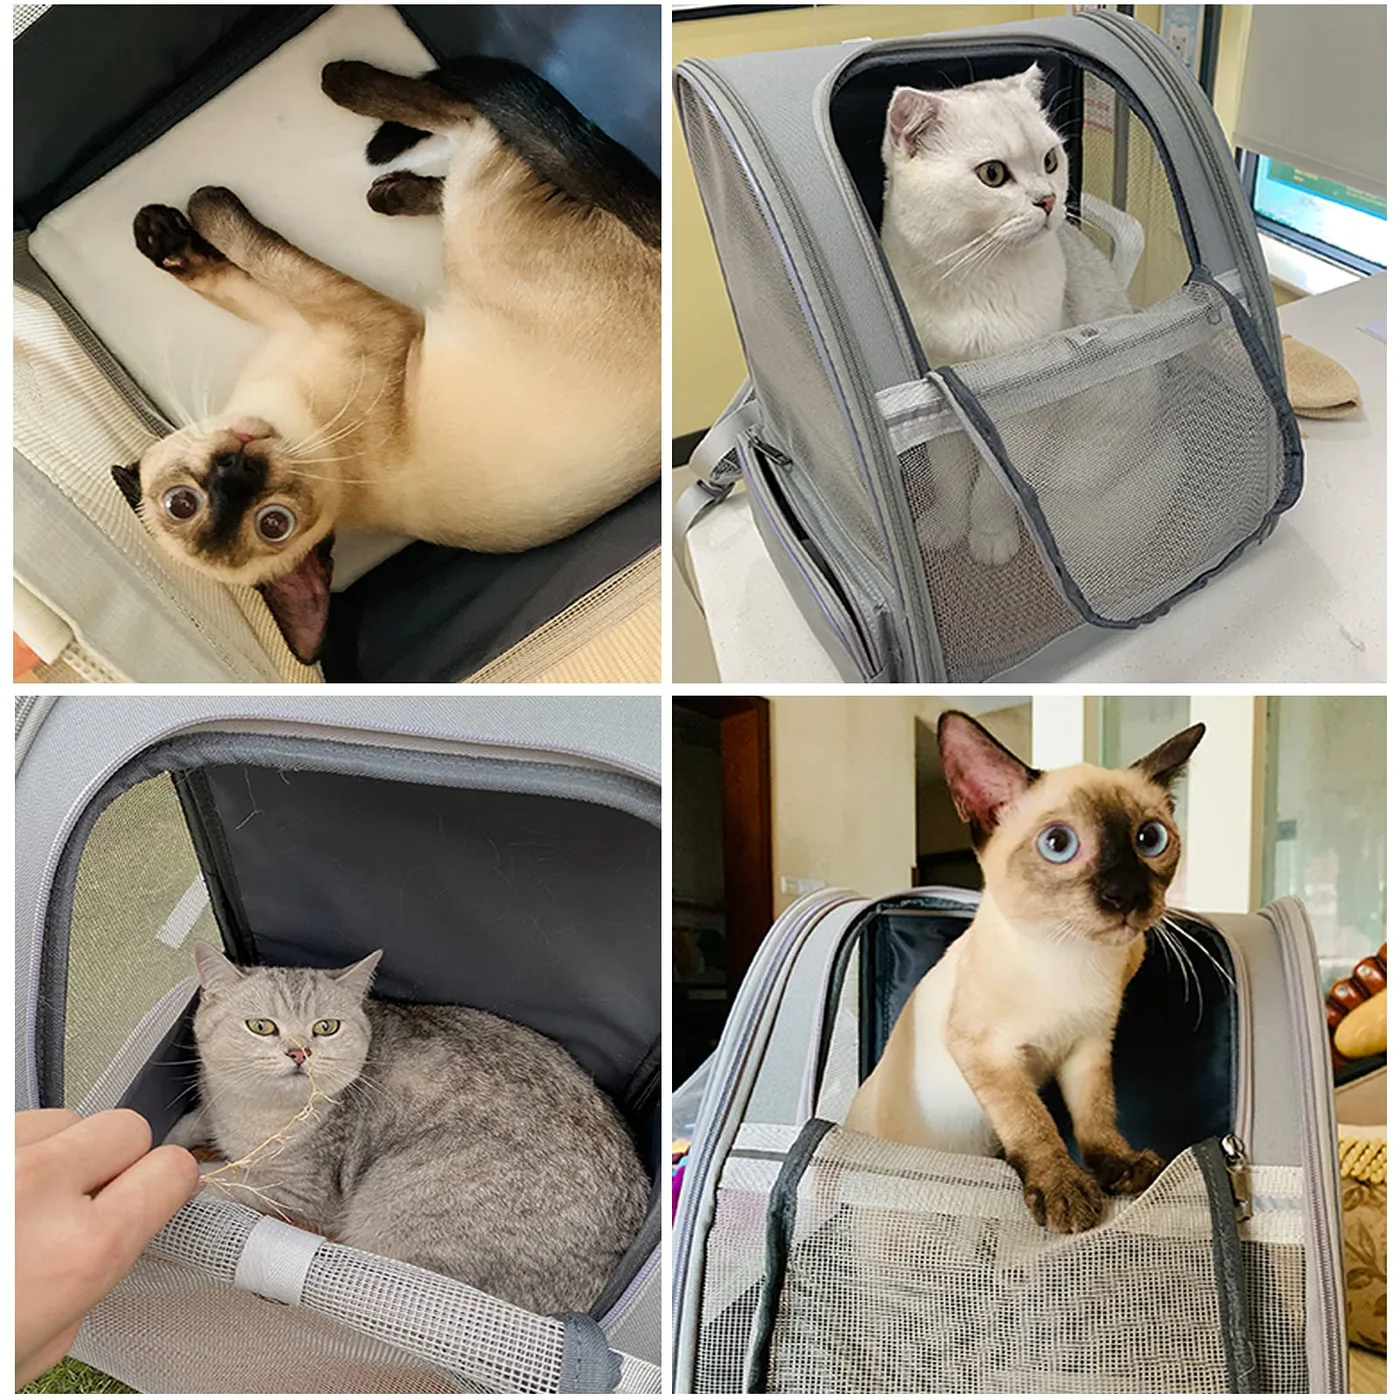
A wholesale dog carrier order and a wholesale cat carrier order rarely share one mould, so the Pet Bag Types & Styles decision has to be locked before tooling money moves. Wholesale pet carriers built on a single shared shell platform let a buyer cover both species from one fabric purchase, which is usually where the first real saving appears.
What a Pet Bag Manufacturer Actually Handles for You
A pet bag manufacturer sits between your brand brief and a finished, carton-packed shipment. That sounds obvious, but buyers routinely confuse three very different commercial models and then wonder why the outcomes differ. The first model is a trading intermediary: it buys whatever is available from several workshops, holds no capacity, and cannot guarantee that your second order matches your first. The second is an assembly workshop: it can sew, but it has no development team, no testing budget and no documentation discipline. The third — the one worth contracting — is a managed manufacturing program, where development, material sourcing, production planning, inspection and export documentation sit under one accountable team.
Our production team operates in that third mode. The difference shows up in the artefacts you receive: a written specification sheet with tolerances, a material confirmation card, a pre-production sample with a dated approval record, an in-line inspection report, a final random inspection report against AQL 2.5, and a packing list that reconciles to the carton marks. If a supplier cannot produce those six documents, you are buying hope, not production.
Capacity is the second thing a manufacturer handles for you. Pet bag demand is seasonal in most markets — Q4 gifting, spring travel, and summer outdoor pushes all compete for the same lines. A manufacturer with 7 dedicated lines and 200,000 pieces of monthly capacity can reserve slots for you; a workshop selling leftover capacity cannot. When you ask for a quotation, ask at the same time which production slot your order would occupy and what happens to that slot if you slip two weeks on artwork approval.
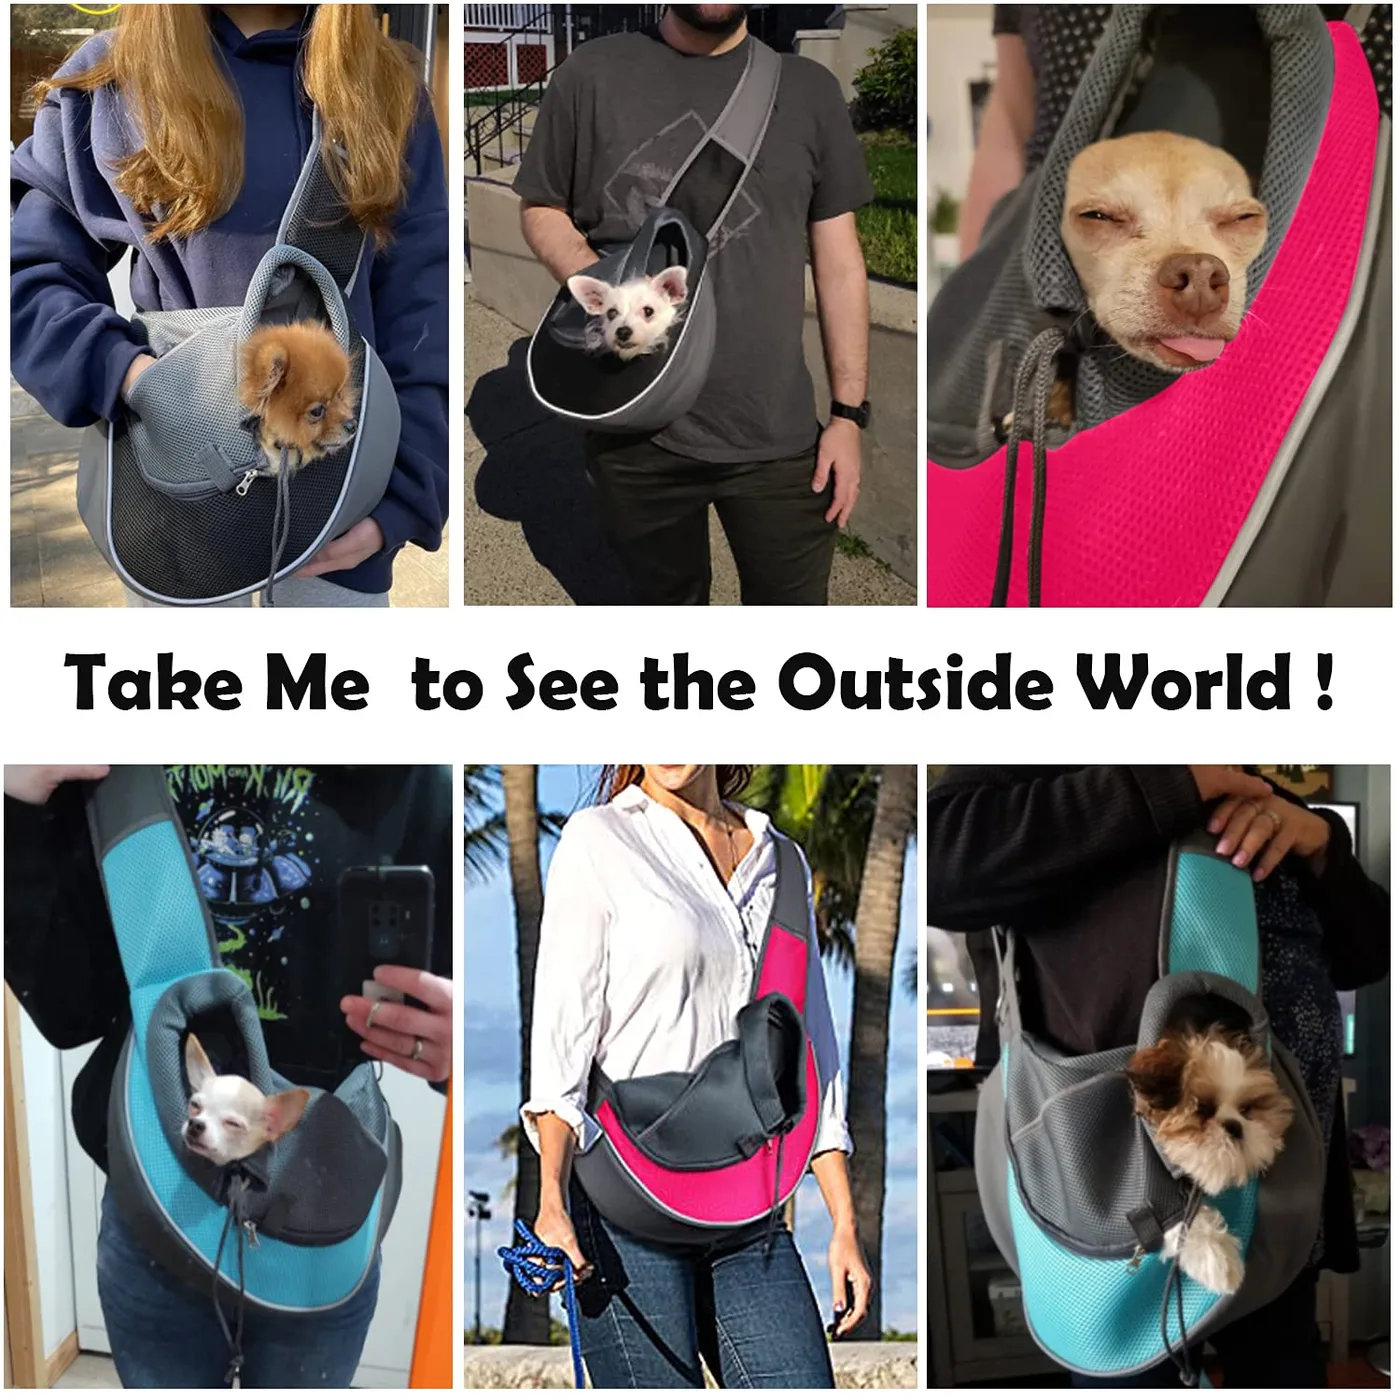
The third responsibility is category coverage. A serious wholesale pet bag program rarely stays in one silhouette. Buyers typically start with one hero SKU, then extend into a travel bag, a tote, a sling and a backpack because retail shelves and online category pages reward assortment depth. Consolidating those four SKUs with one manufacturer reduces your sampling cost per style, lets you share fabric and hardware across the range, and keeps colour standards consistent — which matters more than most first-time importers expect, because a shade mismatch between a tote and a backpack on the same shelf reads as a quality defect to the shopper.
What a manufacturer does not own is worth stating plainly: zipper tape, webbing, buckles, metal hardware and printed labels come from partner facilities that specialise in those inputs. The value of your manufacturing partner is not that it makes every component in-house, but that it holds those partner facilities to a written incoming material standard and pays for the testing that proves it.
Writing the Specification Sheet Before Any Quote
Price without a specification is a guess, and a guess will change the moment the factory understands what you actually want. Before you request a quotation, produce a one-page spec sheet. It does not need to be beautiful; it needs to be unambiguous. Include external dimensions in centimetres with tolerance, internal usable dimensions, empty product weight, recommended pet weight ceiling, shell fabric with denier, lining fabric with coating type, foam or padding specification, mesh specification, webbing width and material, hardware finish, zipper gauge and brand level, closure and safety features, logo method and placement, care and content labelling, and carton pack quantity with carton dimensions.
The most expensive omissions are usually the small ones. Buyers specify "polyester" and receive 300D when they expected 600D. They specify "mesh" and receive a loose knit that fails a claw-snag test. They specify "metal hardware" and receive an untested alloy that fails a nickel-release screen. Each of those gaps becomes a re-sampling round, and each re-sampling round costs you calendar time that no amount of expediting can recover.
| Spec line | Why it moves price and risk | Typical entry for a mid-market program |
|---|---|---|
| Shell fabric | Denier and coating drive both cost and abrasion performance | 600D polyester with PU backing |
| Lining | Coated linings add wipe-clean value and cost | 210D polyester, TPU laminated |
| Padding | Foam density determines shape retention after compression | 8 mm foam, 22 kg/m3 |
| Mesh panel | Ventilation area versus snag resistance | Air-mesh, 3 mm aperture |
| Webbing | Load path; width and weave affect tear strength | 25 mm polyester webbing |
| Hardware | Finish and alloy drive compliance exposure | Zinc alloy, nickel-free finish |
| Zipper | Gauge and brand level drive warranty claims | #5 nylon coil, branded slider |
| Logo | Method changes MOQ, tooling cost and unit price | Woven label plus rubber patch |
| Carton | Pack quantity drives freight cost per unit | 20 pieces, 60 x 40 x 45 cm |
Once the spec sheet exists, request the quotation in two columns: one price at your target quantity, one price at double that quantity. The delta between the two columns tells you how much of your unit cost is fixed setup — pattern making, cutting dies, printing screens, label minimums — and how much is variable material and labour. That single comparison is the fastest way to decide whether to consolidate colours or increase run length, a decision covered in detail in our wholesale pet bags bulk buying guide.
How Unit Price Is Built: Cost Structure Line by Line
A wholesale pet bag quote is not a single number with a margin on top; it is a stack of roughly eight cost blocks. Understanding the stack is what separates a buyer who negotiates intelligently from one who simply asks for a discount and gets it taken out of the fabric.
Material is usually the largest block, typically 45 to 60 percent of the ex-works price for a soft pet bag. Within material, shell fabric dominates, followed by lining, foam, mesh, webbing, hardware and zippers. Hardware and zippers are the two lines most sensitive to specification: moving from an unbranded #5 coil to a branded #8 zipper can change unit cost by a meaningful double-digit percentage on a small bag, and moving from plastic to a nickel-free metal buckle set can do the same.
| Cost block | Share of ex-works price | Main lever available to the buyer |
|---|---|---|
| Shell and lining fabric | 28-38% | Consolidate colourways to reach fabric purchase minimums |
| Hardware and zippers | 12-20% | Standardise finishes across the range |
| Foam, mesh, webbing | 8-14% | Specify by performance, not by brand name |
| Cutting and sewing labour | 14-22% | Reduce panel count and stitch complexity |
| Printing, labels, packaging | 5-10% | Share print screens across SKUs |
| Tooling and sampling setup | 2-6% amortised | Commit to repeat runs so tooling amortises |
| Testing and certification | 1-4% | Test by material family, not by every SKU |
| Factory overhead and margin | 10-16% | Volume commitment and schedule reliability |
Labour is the second large block, and it is driven by panel count and stitch complexity rather than by bag size. A 40 cm tote with eleven panels, bound internal seams and a lined pocket can cost more to assemble than a 50 cm travel bag with six panels and a single straight bind. This is why experienced buyers bring the factory in during design: a reduction of three panels and one pocket often saves more per unit than any negotiation on hourly rate, and it improves first-pass yield at the same time.
Tooling and setup are the blocks that behave strangely for new programs. Cutting dies, embroidery cards, print screens, moulded pullers and branded zipper sliders all carry minimum order quantities from the upstream supplier, often far above your own MOQ of 500. If you commit to a repeat program, these costs amortise across multiple runs; if you treat every order as a one-off, you will pay setup again and again and conclude, wrongly, that your supplier is expensive.
Testing and certification are small in percentage terms and enormous in commercial terms. Budget for them explicitly, and note that most destination markets accept testing by material family rather than by every individual style, provided the construction is equivalent. Ask your supplier to propose a test matrix rather than accepting a per-SKU testing quote — this is one of the easiest savings available to a new importer, and third-party verification through SGS remains the format most retail compliance teams expect to see.
MOQ, Colourways and the Order Quantity Decision
MOQ 500 pieces per colour is the standard entry point for a managed pet bag program, and the number is not arbitrary. It is set by the upstream material chain: fabric dye lots, webbing runs, zipper tape orders and printed label minimums all have their own thresholds, and 500 pieces per colour is the point at which these thresholds stop dominating the unit price.
The practical consequence for buyers is that colourway count is usually a bigger cost driver than total order size. An order of 2,000 pieces in four colours can cost more per unit than 1,500 pieces in two colours, because the four-colour order triggers four dye lots, four label runs and four cutting setups. If your brand needs breadth, buy breadth through silhouettes rather than colours in the first season, then add colours once volume justifies them.
There is a second reason to treat 500 per colour as a floor rather than a ceiling to negotiate below. Below roughly 300 pieces, line changeover time becomes a disproportionate share of the job, quality variance rises because operators have less time to settle into the rhythm of the style, and the factory has little commercial incentive to reserve a slot for your repeat. Buyers who push hard for 200-piece trial runs frequently discover that the trial price is 40 percent above program price, and then draw the wrong conclusion about the supplier.
Where a genuine market test is needed, the better structure is a paid development sample followed by a 500-piece first run in a single neutral colour, with fabric and hardware specified so that the second run can introduce colour without changing the bill of materials. That keeps your first run at standard commercial terms, keeps your second run cheap, and produces clean comparable sales data.
Order quantity should also be read against freight economics. A 20-foot container holds a very different piece count for a flat-packed sling than for a framed travel bag, and shipping a half-empty container is one of the most common hidden costs in a first import. Ask for carton dimensions and a container loading estimate at quotation stage, not after production, and let that estimate inform whether you order 500 or 900.
Sampling: Timeline, Revision Rounds and Approval Gates
Development sampling takes 6-10 working days for a standard soft pet bag, measured from confirmed specification and artwork to a finished sample in hand. The range exists because sampling is not one activity but four: pattern development, material gathering, first build, and internal quality check with photography. A simple tote with stock fabric lands at the short end; a structured travel bag requiring a new foam insert, a new webbing colour and a printed lining lands at the long end.
Buyers lose time in two predictable places. The first is artwork: vector files, colour call-outs in Pantone or a physical swatch, and placement dimensions should be delivered with the specification, not after the first build. The second is undefined approval criteria. If you have not said what "approved" means, every stakeholder will find something to change, and each change restarts the clock.
A workable approval gate has three named outcomes. Approve: the sample matches the spec sheet, and production may begin on receipt of deposit. Approve with noted changes: production may begin only after a written confirmation that the noted changes are costed and scheduled. Reject with cause: a revised sample is required, and the specification sheet is amended before the next build. Requiring a written amendment before a rebuild is the single discipline that prevents sampling drift, defined here as the slow accumulation of undocumented changes that eventually makes the production sample and the contract sample different products.
Plan for two rounds, budget for three. The second round usually exists because a real decision-maker — a retail buyer, a compliance officer, a marketplace category manager — sees the sample for the first time and raises a requirement that was never in the original brief. Expecting this and building slack into your calendar is far cheaper than fighting it later.
Samples should also be treated as the reference standard for production. Keep one sealed approval sample at your office and one at the production base, photographed together at approval, and reference the sample date in the purchase order. When a dispute arises about shade, stitch density or hand feel, a dated physical reference resolves in an hour what a written description never will.
Capacity Planning and Bulk Lead Time Control
Bulk production takes 35-50 days from sample approval and deposit to goods ready for shipment. The variable part is almost never sewing; it is material lead time and line scheduling. Standard shell fabrics and webbing are held in stock by partner facilities, but a custom-dyed colour, a printed lining or a specialised mesh adds one to three weeks before cutting can start.
Understanding this changes how you manage the schedule. If your launch date is fixed, the decision that protects it is not "rush the sewing" — sewing is the shortest and most controllable segment. The decision that protects it is locking materials at the same moment you approve the sample, so that fabric booking and production booking run in parallel rather than in series.
Seasonality is the second scheduling risk. Peak booking for pet bag programs clusters ahead of Q4 retail and ahead of the northern hemisphere travel season, and lines fill in the order that deposits are received, not in the order that inquiries are made. A buyer who approves samples in March for an August delivery will have a quiet, well-priced slot. A buyer who approves in June for the same delivery will compete for capacity and may pay for air freight later to recover the schedule.
Capacity should be read at the program level, not the order level. With 7 lines, 149 machines, 137 staff and roughly 200,000 pieces of monthly output, our production team can hold a recurring slot for a buyer with a published forecast even when individual orders fluctuate. Buyers who share a rolling 90-day forecast receive better slot protection than buyers who issue each purchase order cold — a difference that costs nothing to obtain and is worth weeks in peak season.
Finally, build the schedule backwards from the compliance calendar, not from the desired shelf date. Testing, documentation and import clearance are on the critical path for regulated markets, and a production delay of five days can become a market-entry delay of five weeks if it pushes a shipment past a testing slot or a retail submission window.
Inspection Protocol: AQL 2.5 and Pre-Shipment Checks
AQL 2.5 is the default final random inspection level for wholesale pet bag programs, and the number defines how many defective units are tolerable in a statistically drawn sample before the shipment is rejected or reworked. It is a general consumer-goods inspection standard, not a pet-specific safety standard, and buyers should understand exactly what it does and does not cover.
AQL 2.5 with a normal inspection plan sorts defects into three classes. Critical defects — a broken safety clip, a sharp exposed edge, a functional failure of the load-bearing strap — have an acceptance number of zero. Major defects, such as a visibly misaligned panel, a failed zipper run or a stained lining, are counted against the 2.5 threshold. Minor defects, such as a loose thread or a slight shade variation between panels, are counted against a looser threshold, typically 4.0. A shipment passes only when all three classes are within their limits.
Final inspection is the last gate, not the only gate. A managed program also runs incoming material checks on fabric, webbing and hardware, and an in-line inspection during the first day of cutting and the first hundred pieces of sewing. In-line inspection is where costly problems are caught: a pattern error discovered at piece 80 costs a few hours, while the same error discovered at final inspection costs the entire run.
Buyers should also stipulate the inspection conditions in the purchase order: inspection at the production base before loading, sampling by carton across the full production rather than from a single convenient pallet, a written report with photographs, and no release of balance payment until the report is accepted. Third-party inspection is available and is worth the fee for first orders and for any program above roughly 5,000 pieces.
Where the destination market requires it, pair inspection with laboratory testing on the same lot. Physical inspection confirms that the bag is well made; laboratory testing confirms that the materials are lawful to sell. Both are needed, and neither substitutes for the other — a point that retail compliance teams increasingly enforce, supported by frameworks such as ISO 9001 quality management on the process side and standards bodies such as ASTM International for test method definitions.
Compliance Files and Market Access Requirements
Market access for pet bags is mostly a documentation exercise, and the documentation list is short enough to plan around. For the United States, expect CPSIA general-use provisions, and California Prop 65 assessment if you sell into that state. For the European Union, expect REACH substance restrictions and, where textiles contact skin, an OEKO-TEX certificate on the fabric. For retail and marketplace channels, expect a BSCI or equivalent social-compliance audit on the production base, and increasingly a documented ISO 9001 quality system.
Two principles keep compliance costs under control. First, test by material family: one fabric in four colours does not require four fabric tests, provided the base cloth and finish are identical and the dye house is named. Second, test early: a failed lead-content screen discovered after bulk production is a write-off, while the same screen run at material confirmation stage is a supplier change.
Documentation that should be specified in the purchase order includes a material declaration per component, a test report list with report numbers and validity dates, a country-of-origin statement, a packing declaration, and the care and content label artwork for approval before bulk. Requiring label artwork approval as a separate gate is worth the extra two days; mislabelled fibre content is one of the most common causes of marketplace listing removal and retail chargebacks.
Buyers entering airline-adjacent categories should treat the airline rules as a design constraint rather than a marketing claim. The IATA Live Animals Regulations govern in-cabin animal transport, and individual airline policies are stricter. If a product is positioned for air travel, the specification should be written against the strictest airline in the target market, and the claim should be limited to what the dimensions actually support.
Finally, keep the compliance file alive after launch. Test reports expire, dye houses change, and hardware suppliers substitute. A program that re-tests annually at material-family level and re-validates after any material change will not be surprised by a marketplace compliance request, one of the fastest-growing reasons for listing suspension in the pet category.
Incoterms, Payment and Freight Booking
FOB Xiamen is the default Incoterm for most programs, and it is the right default for a buyer who has any freight capability at all. Under FOB, risk and cost transfer at the point the goods are loaded on board, and the buyer controls the ocean carrier, the routing and the destination charges. Control matters because destination charges are where unexpected cost usually appears.
T/T 30/70 is the standard payment structure: 30 percent deposit to book materials and reserve the production slot, 70 percent balance against the passed inspection report before release of the original documents. This structure aligns incentives correctly — the factory is paid for materials before it commits them, and the buyer retains leverage until the goods are verified. Buyers new to a supplier sometimes ask for payment after receipt; experienced buyers instead ask for a stronger inspection clause, because inspection is what actually protects them.
Where a buyer prefers a landed quote, CIF or DDP is available, but understand what you are buying. Under a landed term the supplier prices in freight risk and destination handling, and you lose visibility of the actual charges. Many importers run a hybrid: FOB for the first two orders while they learn the true cost of freight and clearance, then a landed term once they have benchmark data and can evaluate the quote properly. The ICC Incoterms rules define these allocations precisely and are worth reading once before negotiating.
Freight booking should start when production is roughly sixty percent complete, not when it finishes. Carton dimensions and piece count are confirmed by then, container space in peak season should be booked ahead, and documentation preparation runs in parallel with the last weeks of production. Buyers who wait for a "goods ready" email routinely add two weeks of dwell to a perfectly on-time production schedule.
Put the commercial terms in one place — Incoterm and named port, payment schedule, inspection level and who pays for it, testing responsibility, penalty or remedy for late delivery, and the validity window of the quotation. A quotation valid for thirty days with a named material basis protects both sides from commodity swings and is the mark of a supplier that plans rather than improvises.
Tooling, Moulds and the One-Off Charges Behind a New Style
Every pet bag style that departs from stock components carries a set of one-off charges, and buyers who meet them for the first time at quotation stage usually react to the number instead of the structure. Tooling on a soft pet bag programme rarely means a mould for the bag itself. It means the hardware and branding elements that cannot be produced from existing tools: a buckle or slider body, a rubber or silicone logo patch, a zinc-alloy puller, an embossing or heat-transfer plate, a screen or film set for a printed lining, and a cutting die where a panel shape is not a standard rectangle.
The decision framework is arithmetic. A tooling charge of T spread across a first order of N units adds T divided by N to the unit cost, and the same tooling carried into a second order halves the effective burden. At MOQ 500 pieces per colourway, a tooling line amortises slowly, which is exactly why tooling-heavy branding is a poor fit for a first 500-piece run and a reasonable fit for a 3,000-piece run of the same style. Where the documented step between 500 and 3,000 pieces is roughly 10-14 percent on unit price, the tooling contribution is a separate, non-recurring line that behaves differently from material or labour cost.
| Component | Tooling type | Applies when | Buyer decision |
|---|---|---|---|
| Buckle or slider body | Injection mould | Stock hardware does not meet size or finish | Use stock hardware for the first run |
| Rubber or silicone logo patch | Compression mould | Logo needs a raised, durable mark | Accept; amortises well across repeats |
| Metal zipper puller | Die-cast mould | Brand-level hardware is required | Compare against stock puller plus woven label |
| Printed lining or panel | Screen or film set | Artwork covers a full panel | Limit to one print position in season one |
| Shaped panel | Cutting die | Silhouette is not rectangular | Usually bundled into the sample build |
Ownership and modification clauses matter more than the price of the tooling. Three points belong in writing: who owns the physical tool, whether an idle tool is held or scrapped after a defined period, and what a modification costs. A modification is not free and it is not instant. A revised buckle cavity or a resized plate typically re-enters the same cycle as a new tool, adding one to three weeks before cutting can start, which is the same window a dyed-to-order colour adds to the material chain.
Avoiding tooling altogether is a legitimate first-season strategy, and it is cheaper than most buyers assume. Specifying stock buckles, stock sliders and a woven label instead of a moulded patch removes the one-off cost entirely and shortens the path into the 6-10 working day sample window, because the sample build no longer waits on a tool. Once a style proves itself at 500 pieces and the second order moves toward 3,000, the same tooling can be introduced on a repeat where the amortisation is defensible.
Our production team records every tool under a change-control procedure consistent with ISO 9001, with the tool number, the revision level and the owning style referenced on the specification sheet. That record is what allows a repeat order to run from the revised tool rather than the original, and it is what our vetted partner facilities are checked against under BSCI whenever hardware is produced outside our SGS-verified production base.
Colour Matching: Pantone Targets, Light Booths and Fastness Limits
Colour is the most argued-about line on a pet bag specification and the least documented. A Pantone reference is a target, not a match guarantee: the same Pantone code rendered on a 600D polyester shell, on a coated 210D lining, on 25 mm webbing and on a rubber patch will read differently, because substrate, dye class and surface finish all shift the result. A buyer who writes a Pantone code into a spec sheet without a substrate list has not specified a colour; they have specified an argument.
The workable method has four steps. First, nominate the reference system: Pantone TCX for dyed textile, TPX or a physical swatch where the substrate is coated or printed. Second, agree a numeric tolerance instead of an opinion, and accept a lab dip only when the measured colour difference against the approved standard falls within a defined delta E value. Third, name the light source. D65 is the standard daylight condition, while TL84 and F illuminants represent typical retail and store lighting. Approving under office fluorescent and then selling under halogen is how metamerism disputes begin. Fourth, record the dye lot reference so that the second order is matched to the first production lot rather than to the original chip.
Fastness is a separate specification from shade, and it is where most pet bag complaints actually originate. A shade can be perfect on day one and unacceptable after one wash cycle or one summer of sunlight, which is why the shade approval and the fastness approval should never be signed off together.
| Property | Standard | Typical acceptance for a wholesale programme |
|---|---|---|
| Colour fastness to washing | ISO 105-C06 / AATCC 61 | Grade 4; grade 3-4 accepted on deep shades |
| Colour fastness to rubbing (crocking) | ISO 105-X12 / AATCC 8 | Grade 4 dry, grade 3-4 wet |
| Colour fastness to light | ISO 105-B02 | Grade 4 for outdoor and travel styles |
| Colour fastness to perspiration | ISO 105-E04 | Grade 4 on strap and handle contact areas |
| Print durability | AATCC 61 on the printed composite | No cracking or measurable shade loss after the agreed cycles |
Print method changes the fastness profile, so the print route belongs on the spec sheet alongside the base colour. Sublimation bonds into polyester and performs well on wash and rub; heat transfer sits on the surface and is more vulnerable to abrasion on high-contact panels; screen print builds a layer that can crack across a fold. Where a printed lining or panel is required, our production team runs the fastness test on the printed composite rather than on the base fabric, because testing the base alone proves nothing about the finished article.
Two further points belong in writing. Store the approved lab dip and the production shade standard together, and re-issue both to the dye house on every repeat, because a reference that lives only in a photograph will drift. And re-test whenever the substrate changes: a shade approved on one fabric weight is not automatically approved on a lighter one, even under the same Pantone code.
Finally, connect colour back to the quantity decision. Each colourway is a separate dye lot with its own minimum, which is why MOQ 500 pieces per colourway is the standard entry point and why a four-colour first season costs more per unit than a two-colour one. If the range needs breadth, buy breadth through silhouettes in season one, hold the approved lab dips on file, and release the second and third colourways once a single style has volume behind it.
Retail Packaging, Barcodes and Carton Mark Specifications
Packaging is specified last and fails first. Two distinct packaging routes exist in a wholesale pet bag programme, and mixing them silently is a common and expensive error. Retail packaging is built for a shelf: individual polybag, printed hangtag or header card, a retail barcode on the outside of the pack, and usually a size or feature call-out. E-commerce packaging is built for a fulfilment centre: plain or labelled polybag, a suffocation warning where the destination requires it, a scannable barcode on every sellable unit, carton-level labelling, and pack quantities chosen to match the receiving rules of the destination warehouse rather than a shelf plan.
Barcodes deserve a decision before artwork is locked. A GTIN obtained through your national GS1 member organisation is the only identifier that belongs to an own-brand programme; a number supplied by a supplier or generated by an online tool will not resolve in a retailer or marketplace catalogue, and re-labelling cartons at destination costs several times more than getting it right at packing. Confirm the symbology with the destination channel, then require a scan test on a printed sample before bulk packing begins.
Carton marks are the second half of the same problem. A shipping mark set has two parts: the main mark, printed on the two largest faces, and the side mark, printed on the two narrow faces. Both should carry the identifying core data so that a carton can be recognised from any orientation on a pallet.
| Field | Main mark | Side mark |
|---|---|---|
| Consignee and destination port | Yes | No |
| Purchase order and style number | Yes | Yes |
| Colourway and size | No | Yes |
| Quantity per carton | Yes | Yes |
| Carton number (x of y) | Yes | Yes |
| Gross and net weight | Yes | Yes |
| Carton dimensions | No | Yes |
| Country of origin | Yes | Yes |
The packing list must reconcile to the marks exactly: the same style numbers, the same colourway codes, the same carton numbering, and a total that matches the commercial invoice. Where a retailer requires an advance shipping notice, the carton numbering on the packing list is the source data, and any mismatch becomes a receiving charge at destination rather than a conversation.
Physical performance is the part buyers skip. Cartons for pet bags are frequently tall and relatively light, which makes them vulnerable to crushing in a container rather than to dropping in a warehouse. Specify carton grade by ply and by burst or edge-crush strength, then validate with a drop test performed to ASTM D5276 on a loaded carton from the actual production pack. Our production team runs this on the first bulk pack of a new style and files the result with the ISO 9001 record for that order, so a damage claim can be traced to a tested specification instead of an opinion.
Packaging minimums interact with MOQ 500 pieces per colourway. A printed hangtag, a printed polybag and a printed carton each carry their own run minimum, and a short colourway can force a buyer to over-order printed packaging that is later scrapped. Where a first season runs two colourways, the cheapest correct answer is often a single generic outer carton with the colour identified on the side mark and on the unit barcode, rather than one printed carton per colourway.
Packing also has a schedule. Carton packing runs alongside sewing across 7 lines with roughly 200,000 pieces of monthly output, so a packaging change raised after packing starts does not affect one carton, it affects a shift. Freeze packaging artwork at the same gate as the product specification.
Why First Orders Fail, and When to Add a Second Source
First orders in wholesale pet bags rarely fail on price. They fail on one of five mechanisms, and each mechanism is detectable at a specific point in the programme if somebody is looking for it at that moment.
The first is specification drift: the sample that was approved and the unit that was produced differ, because changes were agreed in messages rather than amended on the specification sheet. The second is material substitution, where a fabric, webbing or hardware item was swapped after costing because the original was unavailable at the booked price, and nobody re-tested. The third is colour divergence, governed by shade tolerance and dye lot control. The fourth is packaging and barcode failure, which damages nothing and blocks the receipt anyway. The fifth is a capacity promise made without a deposit and therefore without a booking.
| Failure mode | First detectable at | Control that prevents it | Cost if missed |
|---|---|---|---|
| Specification drift | Pre-production sample | Written amendment before any rebuild | One re-sampling round and a schedule slip |
| Material substitution | Incoming material check | Material confirmation card plus re-test on any change | Compliance exposure, recall risk |
| Colour divergence | Lab dip and first-off comparison | Numeric delta E tolerance and stored dye lot reference | Chargeback and markdown |
| Packaging or barcode failure | First packed carton | Scan test and packing list reconciliation before bulk packing | Re-labelling at destination |
| Capacity over-promise | Production slot confirmation | Deposit-linked slot booking | Air freight, missed launch window |
The discipline that turns a failed first order into a working programme is a written corrective action record. Under an ISO 9001 framework that means four elements in one document: the nonconformance stated in measurable terms, the root cause rather than the symptom, a corrective action with a named owner and a date, and a verification step that proves the action worked on the next run. A supplier who answers a defect claim with an apology and a discount, without those four elements, will repeat the defect.
A second source is the structural answer to recurring supply risk, but it is not free and it is not always correct. Dual sourcing works when annual volume supports two full MOQ 500 pieces per colourway runs, because splitting a single 500-piece order across two production bases produces two sub-scale runs, two sets of line changeover cost, and two chances of shade divergence. It also forces the tooling question: either duplicate the tooling, which is a second one-off charge, or standardise on stock components so that no tool has to move.
Where dual sourcing is justified, qualify the second base on exactly the same artefacts as the first: the same specification sheet with tolerances, the same approval sample held on both sides, the same AQL 2.5 final random inspection drawn to ISO 2859-1, and a BSCI-audited partner facility wherever components are made outside our SGS-verified production base. Run an allocation rather than a switch, giving the second source a defined share of volume while it proves itself, then review on defect rate, on-time rate and shade consistency before reallocating.
Not every programme needs one. Below roughly two repeat orders per year on a style, the cost of duplicate qualification usually exceeds the risk it mitigates, and the better investment is a rolling forecast shared with one accountable production team. Our SGS-verified production base runs 4,950 square metres with 7 lines, 149 machines and 137 people, supporting roughly 200,000 units of monthly output; reserving a slot inside that capacity through a shared forecast buys more protection than a second qualification bought in a hurry.
Production capability
- SGS-verified production space of 4,950 m², 149 machines, 7 assembly lines
- Pet bag output since 2014 from a 137-person team
- 200,000 units shipped monthly under BSCI and ISO 9001 systems
People Also Ask
How do I verify a pet bag manufacturer before placing an order?
Ask for six artefacts: a written specification sheet with tolerances, a material confirmation card, a dated pre-production sample approval, an in-line inspection report, a final AQL 2.5 report, and a packing list that reconciles to the carton marks. A supplier that cannot produce all six is trading stock rather than running a managed program.
Why is the MOQ 500 pieces per colour?
The 500-piece threshold is set by upstream suppliers rather than by the sewing line. Fabric dye lots, zipper tape orders, webbing runs and printed label minimums all carry their own quantities, and 500 pieces per colour is roughly where those thresholds stop dominating unit cost.
What is included in a pet bag manufacturing quote?
A usable quote breaks out material, hardware, labour, printing and packaging, tooling or setup, testing and overhead, and states the Incoterm, validity window and material basis. Requesting the same quote at two quantity levels shows how much of the unit price is fixed setup cost.
How early should I book freight for a pet bag shipment?
Book freight when production is roughly sixty percent complete, because carton dimensions and piece counts are confirmed by then and peak-season container space must be reserved ahead. Waiting for a goods-ready notice typically adds about two weeks of dwell time to an otherwise on-time schedule.
What documents are needed to import pet bags into the US or EU?
Expect a material declaration per component, test reports with numbers and validity dates, a country-of-origin statement, a packing declaration and approved care and content label artwork. US imports also consider CPSIA and California Prop 65, while EU imports consider REACH and often OEKO-TEX for skin-contact textiles.
How do I keep quality consistent across repeat orders?
Keep a sealed approval sample at both your office and the production base, photograph them together at approval and reference the sample date in every purchase order. Re-test annually at material-family level and re-validate after any change of dye house or hardware supplier.
Frequently Asked Questions
What is the minimum order quantity for a pet bag program?
The standard MOQ is 500 pieces per colour for a managed program. The threshold is set by upstream material minimums such as fabric dye lots, zipper tape runs and printed label orders, so ordering below it usually raises unit cost rather than lowering risk.
How long does sampling take?
Development sampling takes 6-10 working days from confirmed specification and artwork to a finished sample. Simple constructions using stock fabric land at the short end of the range; structured styles needing new foam inserts, printed linings or custom webbing colours land at the long end.
What is the bulk production lead time?
Bulk production takes 35-50 days from sample approval and deposit to goods ready for shipment. The variable portion is material lead time and line scheduling rather than sewing, so locking materials at sample approval is the most effective way to protect a fixed launch date.
What does AQL 2.5 mean for my shipment?
AQL 2.5 is the acceptable quality limit used for the final random inspection, defining how many major defects are tolerable in a statistically drawn sample. Critical defects such as a failed load-bearing strap or a sharp exposed edge have an acceptance number of zero regardless of the AQL level.
Do you own the factory that produces my order?
Production is managed by our production team across an SGS-verified production base of 4,950 square metres plus partner facilities that specialise in components such as zippers, webbing and metal hardware. What we contract for is a single accountable program covering development, material control, inspection and export documentation.
Which certifications does the production base hold?
The production base holds BSCI social compliance and ISO 9001 quality management certification. Third-party laboratory testing for CPSIA, REACH, Prop 65 and OEKO-TEX is arranged through SGS where the destination market or the retail channel requires it.
Can I test one fabric instead of every SKU?
Yes, most markets accept testing by material family when the base cloth, finish and dye house are identical and the construction is equivalent. Testing by material family rather than by every individual style is one of the simplest ways to control compliance cost in a first season.
What payment terms apply?
Standard terms are T/T with 30 percent deposit to book materials and reserve the production slot, and 70 percent balance payable against a passed inspection report before release of the original shipping documents.
Which Incoterm should a first-time importer choose?
FOB Xiamen is the sensible default for a first-time importer because it keeps control of the ocean carrier, routing and destination charges with the buyer. Landed terms such as CIF or DDP are better adopted once you have real freight and clearance data to benchmark the quote.
How is unit price affected by the number of colours?
Colourway count usually moves unit price more than total volume does, because each colour triggers a separate dye lot, label run and cutting setup. Two colours of 750 pieces each will typically price better than four colours of 500 pieces each.
What happens if my artwork is not ready at sampling?
Artwork delays are the most common cause of sampling slip. Vector files, Pantone or physical swatch references and placement dimensions should be delivered with the specification; supplying them after the first build typically adds a full revision round and restarts the sampling clock.
Can I reserve production capacity for a repeat program?
Yes. Buyers who share a rolling 90-day forecast receive better slot protection than buyers who issue each purchase order cold, particularly in peak season ahead of Q4 retail and the northern hemisphere travel period.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample