Shock Absorbing Pet Bags: Impact Protection Sourcing Guide
Shock-absorbing pet bags should be specified by impact attenuation rather than by padding thickness: a competent build reduces transmitted peak acceleration by 40-60% in a standard drop test from 0.8-1.0 metres onto a hard surface, using closed-cell foam or moulded EPP in the 25-45 kg/m³ density band with a structured base insert. Thickness alone is misleading, because a soft low-density foam bottoms out and transmits the full shock while a correctly specified medium-density foam absorbs it. The number to put in a tech pack is peak acceleration transmitted to a test mass.
Impact protection is bought for one reason: to keep an animal uninjured when a bag is dropped, kicked, tipped from a seat or shifted during braking. That is a narrow event with a large consequence, and it is specified the way any protective product is specified - by measuring what is transmitted through the structure rather than by describing the padding. Our production team specifies impact programmes on four numbers: drop height, transmitted peak acceleration, foam density and compression set after repeated loading, and it quotes each build against those numbers rather than against a millimetre of foam. Qualification sampling runs 6-10 working days and includes instrumented drop testing on the finished bag with a representative test mass. Bulk production is 35-50 days from approved sample, inspected to AQL 2.5 with foam density and insert placement verified on the line. Standard terms are MOQ 500 pieces per colourway, T/T 30/70 and FOB Xiamen.
Pet bag market size is reported three different ways depending on whether carriers, travel bags and accessories are bundled, so Material & Technology planning should pick one definition and stay with it. Pet bag market report figures are useful for board decks and of little use for MOQ planning.
Impact Attenuation: Measuring What Actually Matters
Impact protection is a transmission problem. The energy arriving at the bag is fixed by the drop height and the mass; what varies is how much of that energy reaches the animal. The measurable quantity is peak acceleration at the payload, usually expressed in g, and the useful specification is a maximum allowable peak under a defined drop test.
The standard method is an instrumented drop: an accelerometer mounted on a test mass of representative weight, the bag dropped in a defined orientation onto a defined surface, and the peak recorded across a set number of drops. Orientations matter because a bag does not always land on its base: base, side, corner and top drops each produce a different result, and the corner drop is usually the worst because the load concentrates on a small area of padding.
A workable acceptance criterion for a mid-size pet bag is a transmitted peak below a stated g value in all four orientations from a stated height, with no structural failure - no split seam, no broken frame, no closure opening. Structural failure during a drop is arguably more important than the acceleration number, and it is also easier to specify precisely,, because an opened closure is an escape event regardless of how well the padding performed.
Test methods and instrumented drop practice are documented by the standards community, and reports should name the method used: ASTM International publishes cushioning and impact test methods and ISO maintains the management framework that governs how accredited labs document results. A drop test performed in-house without a documented protocol is a demonstration, not a result.
Two protocol details are frequently omitted and both change the answer. The first is recovery time between drops: foam needs time to rebound, and drops delivered in quick succession produce worse results than the same drops spaced apart, so the interval belongs in the protocol. The second is the impact surface, because concrete, steel plate and vinyl-over-concrete produce materially different peaks for the same drop height.
Foam Selection: Density, Cell Structure and Compression Set
Padding performance is governed by density, cell structure and thickness, in that order of importance. Density in kg/m³ determines how much energy a given volume can absorb before it bottoms out. Cell structure determines whether the foam returns: closed-cell foams resist water and hold shape, while open-cell foams breathe and compress more easily. Thickness determines how much travel is available to decelerate the load.
| Foam type | Density band (kg/m³) | Attenuation | Weight penalty | Cost index | Best use |
|---|---|---|---|---|---|
| EPE, low density | 18-25 | 20-30% | Very low | 100 | Light retail totes |
| EPE, medium | 25-35 | 35-45% | Low | 112 | General carriers |
| EVA, closed cell | 35-60 | 45-60% | Medium | 135 | Travel programmes |
| Moulded EPP | 30-45 | 55-70% | Low-medium | 165 | Premium and transit |
| Memory foam laminate | 45-80 | 50-65% | High | 180 | Comfort-led premium |
The instructive failure in this table is the low-density row. A thick pad of 20 kg/m³ foam feels protective in the hand and performs poorly in a drop, because it compresses fully and transmits the rest of the energy directly. Adding thickness to a low-density foam does not fix that; raising density does. This is the single most common specification error in impact programmes.
Compression set is the property buyers forget. Foam that has been compressed repeatedly loses thickness and therefore travel, so a bag that passed a drop test when new may fail after a season of use. Specify a maximum compression set percentage after a defined number of load cycles and verify it on the production foam, not on a sample swatch.
Temperature is the other property that quietly changes the result. Foam stiffens in cold conditions and softens in heat, so a build tuned at room temperature behaves differently in a cold vehicle or a hot terminal. Programmes shipping into wide climate ranges should require drop results at the extremes as well as at standard conditions, or should select a foam whose properties are stable across the range.
Structural Design: Spread the Load Before Absorbing It
Padding works best when the load arrives spread out. A concentrated impact on a corner overwhelms local padding regardless of its quality, while the same energy arriving across a wide panel is easily managed. Structural design that spreads load therefore does more for impact performance than padding specification, and it usually costs less.
Three structural elements do the work. A rigid or semi-rigid base insert distributes a base drop across the whole footprint and prevents the frame from punching through. Corner reinforcement - a moulded bumper, a doubled panel or an internal frame member - converts a corner impact into a panel impact. A suspension or cradle construction decouples the inner floor from the outer shell so the payload is not directly coupled to the impact surface.
- Base insert: prevents punch-through and keeps the footprint flat.
- Corner reinforcement: converts the worst-case orientation into a manageable one.
- Cradle or suspended floor: decouples the payload from the shell.
- Framed top: prevents collapse onto the animal if the bag lands inverted.
Top and side structure deserves attention because inverted and side drops are common in vehicle and transit settings, and a bag that collapses inward transmits load directly onto the animal. A light frame, a stiffened perimeter or an internal hoop keeps the volume open under load and is one of the cheapest protective measures available.
Padding placement should follow the impact map rather than the panel layout. Reinforcing the base and four lower corners typically delivers most of the available protection for a fraction of the cost and weight of padding every panel evenly, because those are the surfaces that actually land first. Our production team builds a placement plan from the orientation weighting before quoting, which is why two quotations for the same foam can differ in both price and performance.
Access is the practical constraint on placement. Foam that improves performance but blocks a pocket, a vent or an opening will be removed by the user or will make the bag unpleasant in daily handling, so the placement plan should be reviewed against the full feature list before it is frozen. The best-performing layout on paper is worth little if it interferes with how the product is used every day. Panel access, vent position and pocket placement should all be checked against the final map before the pattern is cut.
Building a Padding Placement Map
A placement map is a one-page drawing showing where foam of each density goes, at what thickness and with what coverage. It is the document that prevents the most common bulk defect, which is not wrong foam but foam in the wrong place or missing at a corner. Producing it during sampling costs nothing and it becomes the inspection reference for every subsequent season, which is why our production team treats it as part of the approval pack rather than as an optional extra.
The map should also record the attachment method. Foam that is loosely inserted can migrate during use and end up bunched at one end of a panel, leaving the other end unprotected, while bonded or pocketed foam stays where it was placed. Migration is a field failure rather than a bulk defect, so it cannot be caught at inspection and has to be designed out.
Where Impact Events Actually Occur
Impact events in pet bag programmes cluster into five scenarios, and each implies a different dominant orientation. A bag tipped from a car seat lands on a side or corner. A bag set down hard on a terminal floor lands on its base. A bag knocked from a counter lands inverted or on a side. A bag shifted during braking hits the seat frame or footwell. A bag dropped while being carried lands on whatever corner the handler lost first.
Scenario weighting is what makes a specification honest. A programme sold for car use should be tested primarily in side and corner orientations. A programme sold for counter-height handling in clinics should prioritise base and inverted drops. A single-orientation test tells a buyer very little about the product's real behaviour, and a four-orientation test costs marginally more.
Animal size sets the test mass. A bag marketed for animals up to 8 kg should be tested with a representative mass in that range, not with an empty bag and not with a mass at the top of a larger range. Using an unrealistically light test mass is the most common way an impact claim becomes indefensible.
Handling culture is the variable buyers can influence but rarely do. Instructions telling an owner to set the bag down rather than drop it, and to secure it during vehicle travel rather than leave it loose, reduce the frequency of the event more cheaply than any material change. The instruction card is part of the protection system and should be specified alongside the foam.
Transport guidance frames the same issue from the welfare side. IATA maintains the Live Animals Regulations governing air carriage and the American Veterinary Medical Association publishes transport guidance, both of which treat containment integrity and stability during handling as welfare requirements rather than product features.
Inspection data from returned goods points consistently at four locations: the base corner nearest the handle, the zip garage, the shoulder strap anchor and the base panel seam. Padding the centre of a large panel rarely addresses any of them. A padding map that concentrates material at those four points costs less and performs better than uniform thickness throughout, because mass placed where nothing happens is simply freight.
Weight, Bulk and the Commercial Trade-Off
Impact protection competes directly with weight and packed bulk, and both carry commercial costs. Foam and frame members add grams that raise freight per unit across the whole programme, and thick padding adds packed volume that raises the carton cube and therefore the container cost. A padded bag that ships 20% fewer units per container has a landed cost penalty that no amount of material saving elsewhere will recover.
Nested packing and compressible construction are the mitigations. Padding that compresses for shipping and recovers in use reduces cube without reducing protection, and designs that nest reduce both cube and damage in transit. Both should be evaluated during sampling rather than after the carton specification is fixed.
Transit damage is the overlooked part of this trade-off. A padded bag compressed into a tight carton can arrive with permanent foam deformation before it reaches a customer, while one shipped loose but uncompressed arrives scuffed. Specify carton fit and compression limits together, and inspect a shipped carton rather than a hand-carried sample before approving the packing.
| Build | Added weight (g) | Attenuation | Units per 40' container | Landed cost impact |
|---|---|---|---|---|
| No dedicated padding | 0 | < 15% | 2,400 | baseline |
| Medium EPE panels | 120 | 35-45% | 2,180 | +3.1% |
| EVA base + corners | 210 | 45-60% | 1,980 | +6.4% |
| Moulded EPP cradle | 260 | 55-70% | 1,760 | +9.8% |
Read the last column as a pricing decision rather than a problem: roughly 3-10% of landed cost buys a materially safer product and a defensible marketing claim. Most premium programmes find that trade easy; most entry programmes should still take the first step, because it is the cheapest one.
There is a pricing upside that offsets part of the cost. Impact protection is one of the few pet bag features that supports a higher retail price without a corresponding rise in perceived complexity, because buyers can see and feel the padding. Programmes that document the performance on the hangtag recover more of the added cost at retail than programmes that add the padding silently.
Freight is the hidden cost of protection. A padded base and reinforced side walls typically add 180-320 g per unit, which on a 1,500-piece booking translates into roughly a quarter to half a tonne of additional chargeable weight. Buyers shipping by air feel that difference immediately; buyers shipping by sea usually do not, which is why the padding decision should follow the freight mode rather than precede it.
Comfort vs Protection: Two Different Design Goals
Buyers frequently conflate comfort padding with impact padding, and the two are only partly overlapping. Comfort padding is about sustained low-load pressure distribution: soft, conforming, open-cell materials that feel pleasant and reduce pressure points over hours. Impact padding is about transient high-load energy absorption: firmer, resilient, closed-cell materials that decelerate a load over a short distance. A very soft comfort foam can be a poor impact material, and a firm impact foam can feel unyielding.
The resolution in a good design is a laminate: a firmer impact layer bonded to a softer comfort layer, with the firm layer toward the outside. That construction is common in protective equipment generally and it works equally well in pet bags, at a modest cost premium over a single layer.
Thermal behaviour is the second difference. Closed-cell impact foams insulate, which is a benefit in cold transit and a liability in heat. Programmes sold into warm climates should evaluate ventilation alongside padding, because a well-padded bag with poor airflow can create a heat problem that is more dangerous than the impact it prevents.
Cleanability is the third. Open-cell comfort foams absorb liquid and odour; closed-cell foams wipe clean. For any programme involving young animals, long durations or clinical use, closed-cell or a sealed lamination should be specified regardless of the comfort preference.
Removable and washable interiors are the practical answer for programmes that need both. A sealed closed-cell impact shell with a removable, washable comfort liner gives cleanability without compromising the energy-absorbing layer, and it also gives the brand an accessory line. The added cost is modest and it removes the most common cleanliness complaint in padded products.
Odour retention deserves a line in the same specification, because soft interiors are where odour accumulates and the complaint arrives long after the return window. A liner treated for odour control carries its own chemical documentation requirement, so it must be approved with the finish file rather than added at the end of the sampling window.
Verification: Drop Protocol, Sampling and the Acceptance Clause
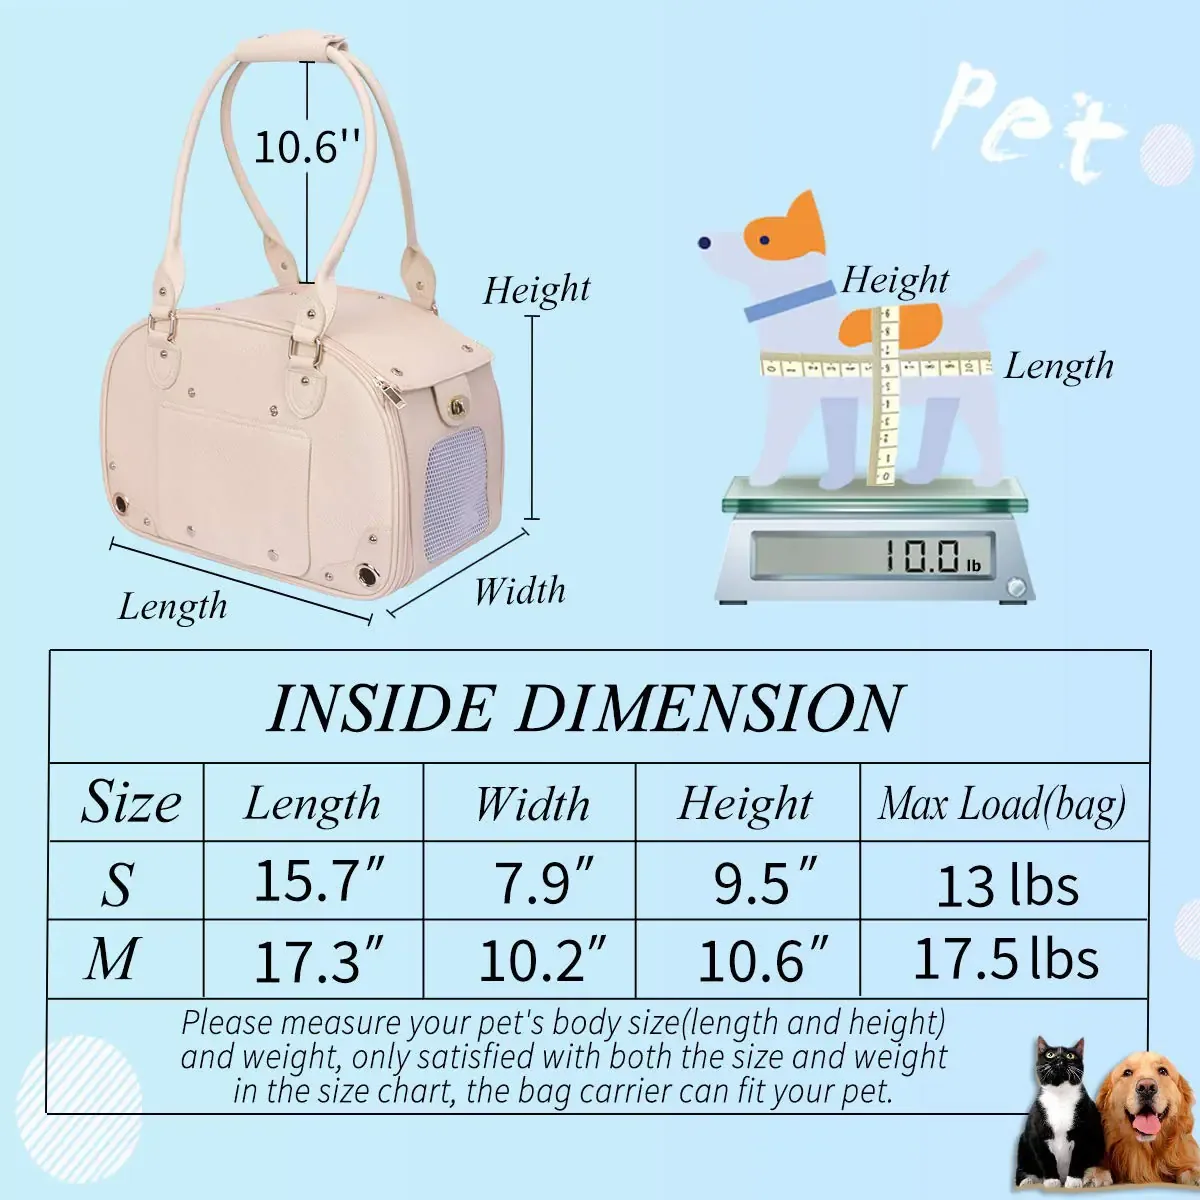
The clause that makes impact protection real has five parts. Written into the tech pack, they convert a description into something a lab can pass or fail and an inspector can act on at goods-in.
- Test protocol: drop height, orientations, surface, test mass and number of drops per orientation, all stated in advance.
- Threshold: maximum transmitted peak acceleration, plus a no-structural-failure requirement including closure integrity.
- Material verification: foam density and thickness measured on the production lot, with a tolerance.
- Durability: maximum compression set after a defined number of load cycles.
- Remedy: lot rejection or documented replacement at the supplier's cost, with a re-test window.
Sampling should acknowledge that padding is assembled rather than extruded. Density and thickness vary across a sheet and with cutting, so three specimens per production batch measured at the thinnest point, with the lowest value reported, is a defensible rule. Measuring a single centre sample from a comfort swatch is how a programme ends up with padding that is nominally correct and functionally thin at the corners.
At goods-in, insert placement matters as much as material. A correct foam installed in the wrong position, missing at a corner, or folded during assembly provides no protection at all. Our production team inspects to AQL 2.5 with missing, displaced or folded inserts classified as critical defects, and verifies density on the line rather than only on the incoming material.
Finally, keep a physical reference. A cut-away sample showing foam placement, density marking and frame position, signed off at approval and retained by both sides, settles placement disputes in minutes. Our production team produces one for every impact programme for exactly that reason.
Write the drop protocol down before sampling, including drop height, orientation, drops per unit, substrate and the pass criterion. Suppliers reading "must survive a drop" will each invent a different test and the results become incomparable. Our production team quotes against the buyer's written protocol rather than supplying our own, precisely so that the comparison means something.
Briefing a Supplier for an Impact-Protected Programme
A complete brief fits on one page: animal weight range, drop height and orientations, maximum transmitted acceleration, foam type with density and thickness tolerance, structural elements required, thermal and cleanability constraints, and the verification protocol with remedy. That is the whole document.
Buyers should also state the claim they intend to make. A product described as impact protected needs the performance file behind it; a product described as padded and comfortable does not. Knowing which wording will appear on the hangtag determines how much testing the programme needs, and deciding it at briefing rather than at copywriting avoids the usual rush to commission tests after the bulk date.
When to Re-Test
Re-test annually, and immediately after any change to foam supplier, density, thickness, frame geometry or carton compression. Padding is the component most likely to be quietly substituted, because a small density change is invisible on a finished sample and only appears in the drop result. A programme that re-tests on those triggers rarely discovers a problem through a customer.
What Sampling Should Produce
Qualification sampling runs 6-10 working days and should produce an instrumented drop report across four orientations, a density and thickness measurement on the production foam, a compression-set result, and a finished sample that has been through all of it. Approving on feel alone is the most common and most expensive shortcut in this category.
Cost and Timing Notes
Bulk production is 35-50 days from approved sample, with additional time if moulded EPP or a custom frame is tooled. Standard terms are MOQ 500 pieces per colourway, T/T 30/70 and FOB Xiamen. Programmes using moulded components should treat tooling as a programme asset and confirm ownership and repeatability terms at quotation.
Questions That Reveal Supplier Capability
Ask what drop height and orientations were tested, whether the test mass matched the marketed animal weight, whether the closure stayed closed during the drop, and whether density was measured on the production lot. Suppliers who answer all four without hesitation have built impact-protected products before; those who describe only foam thickness have not.
Why brands source here
- Pet bag programmes run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
How much impact should a pet bag absorb?
A competent build reduces transmitted peak acceleration by 40-60% in an instrumented drop from 0.8-1.0 metres onto a hard surface, across base, side, corner and top orientations. The specification should state a maximum transmitted peak in g plus a requirement that no seam splits and no closure opens.
Is thicker padding better for impact protection?
Not on its own. Padding performance depends primarily on density, because a low-density foam compresses fully and transmits the remaining energy directly. Raising density from 20 to 35 kg/m³ improves attenuation more than doubling thickness at the low density.
Which foam is best for shock-absorbing pet bags?
Medium-density EPE suits general carriers, closed-cell EVA suits travel programmes, and moulded EPP gives the best attenuation-to-weight for premium and transit use. Comfort-led premium builds often use a firm impact layer laminated to a softer comfort layer.
Why are corner drops the worst case?
A corner impact concentrates the load onto a small area of padding and overwhelms it locally, while the same energy spread across a panel is easily absorbed. Corner reinforcement converts the worst-case orientation into a manageable one.
Does foam lose its protective ability over time?
Yes. Repeated compression causes compression set, which reduces thickness and therefore the deceleration distance available. Specify a maximum compression set after a defined number of load cycles and verify it on the production foam.
How much does impact protection add to landed cost?
Medium EPE panels add roughly 3% to landed cost, an EVA base with corner reinforcement about 6%, and a moulded EPP cradle close to 10%, once extra weight and container cube are included. The first step is the cheapest and usually worth taking.
Is comfort padding the same as impact padding?
No. Comfort padding distributes sustained low-load pressure and is soft and open-cell; impact padding absorbs transient high-load energy and is firmer and closed-cell. A laminate with the firm layer outward delivers both.
Frequently Asked Questions
How is impact protection measured on a pet bag?
With an instrumented drop test: an accelerometer on a representative test mass, the bag dropped from a defined height in base, side, corner and top orientations onto a defined surface, and the peak acceleration recorded. The protocol must be written before testing begins.
What drop height should be specified?
0.8-1.0 metres is the practical range for pet bags, matching counter height, car seat height and carried-handling drops. The height should reflect the programme's real handling scenarios rather than a convenient number.
Should the test mass match the marketed animal weight?
Yes. A bag marketed for animals up to 8 kg should be tested with a representative mass in that range. Testing empty or with an unrealistically light mass is the most common way an impact claim becomes indefensible.
Why does closure integrity matter in a drop test?
Because an opened closure is an escape event regardless of how well the padding performed. The acceptance criterion should include no structural failure, explicitly covering seams, frame and closure, alongside the acceleration threshold.
What is compression set and why does it matter?
Compression set is the permanent loss of thickness after repeated loading. It matters because it reduces the deceleration distance available, so a bag that passed when new can fail after a season of use.
Do moulded EPP components require tooling?
Yes, and tooling lead time sits on top of the 35-50 day bulk window. Buyers should treat mould tooling as a programme asset and confirm ownership, repeatability and re-order terms at quotation rather than at the second season.
Does padding make a pet bag too hot?
Closed-cell impact foams insulate, which helps in cold transit and can be a liability in heat. Programmes sold into warm climates should evaluate ventilation alongside padding and consider ventilation geometry rather than thinner foam.
Can padding be added to an existing design?
Usually yes, but placement matters more than quantity. Panels added at the base and corners improve results substantially; the same foam distributed evenly across all panels does less for more cost and weight.
How should padding be inspected at goods-in?
Verify density and thickness on the production lot at the thinnest point, and confirm that inserts are present, correctly positioned and unfolded. Missing or displaced inserts should be critical defects under AQL 2.5.
Is a rigid base insert worth the added cost?
Almost always. It prevents the frame punching through the padding, keeps the footprint flat so load spreads properly, and improves stability at the same time. It is one of the highest-value structural additions available.
What is the difference between EPE, EVA and EPP?
EPE is a lightweight polyethylene foam suited to general programmes, EVA is a denser closed-cell material with better energy absorption and durability, and EPP is a moulded bead foam offering the best attenuation per gram. Cost and process complexity rise in that order.
How long does qualification sampling take?
6-10 working days, producing a four-orientation drop report, density and thickness measurements on the production foam, a compression-set result and a tested finished sample. Approving on feel alone is the most expensive shortcut in this category.
Talk to QUANZHOU JUNYUAN BAGS about a wholesale pet bag order: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample